Automatic Packaging Film
Engineered Roll Stock for VFFS & HFFS Lines
High-barrier roll stock engineered for high-speed vertical and horizontal form-fill-seal (VFFS/HFFS) lines. Precise COF control, wide heat-seal windows, food-grade materials — FDA, EU 10/2011 and GB compliant, with gravure and flexo printing.
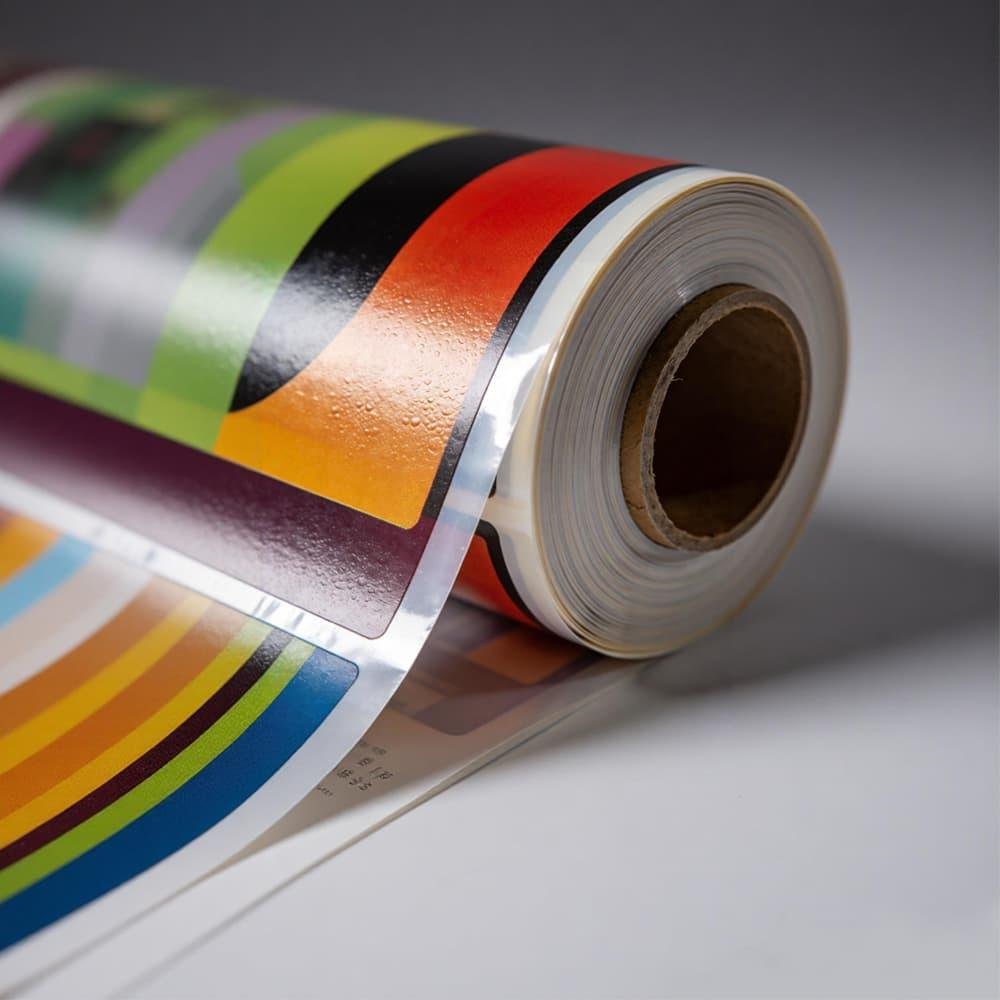
Automatic Packaging Film — Engineered Roll Stock for High-Speed FFS Lines
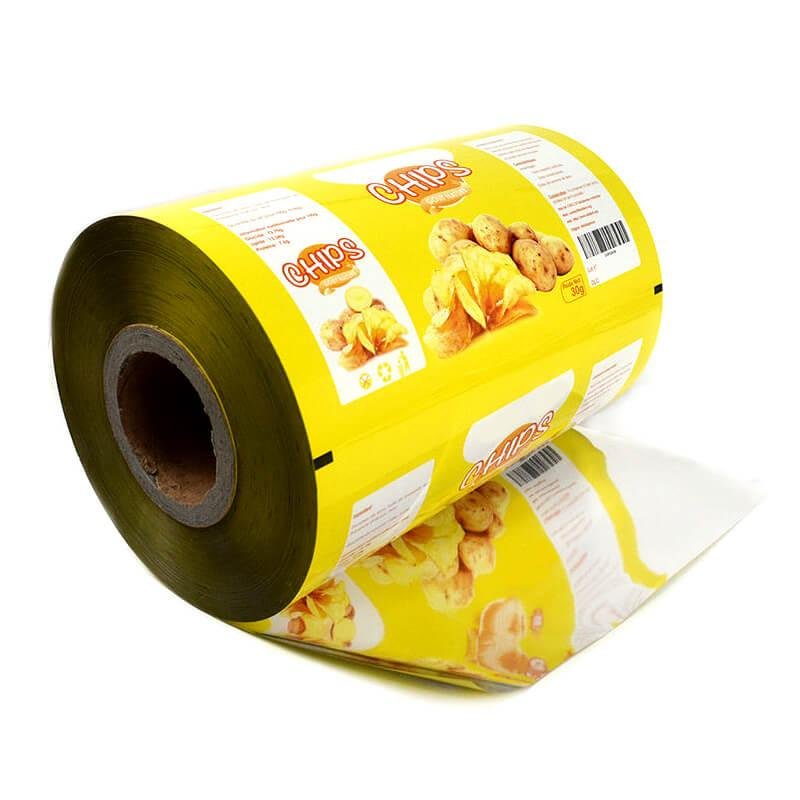
Automatic packaging film — also called roll stock film, FFS film, or VFFS/HFFS film — is a continuous web of engineered flexible material wound onto a core and fed directly into a form-fill-seal machine that folds, fills, and seals each pack in one automated operation. It is the single highest-leverage consumable on your line: the film determines line speed, seal integrity, barrier performance, defect rate, and ultimately your cost per pack.
This page is written for packaging engineers, procurement managers, and operations leaders who specify roll stock for high-speed lines and need to compare suppliers on more than price. What follows is a full engineering and procurement reference: quantified barrier data (OTR/WVTR), coefficient-of-friction and heat-seal specifications, a regulatory compliance matrix, a failure-mode analysis, and a supplier-evaluation checklist.
What You Can Expect From Our Factory
- ISO 9001:2015 quality system with lot-level COF, seal, and barrier test reports on every production run.
- Food-grade structures compliant with FDA 21 CFR, EU 10/2011, and GB 4806.7 / GB 9685.
- Gravure (rotogravure) and flexographic printing up to 10 colors, with Pantone color-matching.
- Low MOQ and 7–15 day lead time on repeat structures.
- Free sample rolls for on-line machine trials before you commit.
Film Structure & Barrier Engineering
Barrier performance is specified by two numbers: oxygen transmission rate (OTR, cc/m²/day) and water-vapour transmission rate (WVTR, g/m²/day). Both are meaningless without test conditions — OTR is typically measured at 23 °C / 0% RH (ASTM D3985), WVTR at 38 °C / 90% RH (ASTM F1249). The same film tested at 23 °C / 50% RH can report an OTR up to 3× higher. Always confirm the condition before comparing two supplier datasheets.
| Film Structure | Typical OTR (cc/m²/day) | Typical WVTR (g/m²/day) | Seal Strength (N/15 mm) | Recyclability | Typical Application |
|---|---|---|---|---|---|
| PET / Al foil / PE (3-ply) | < 0.01 | < 0.01 | 30–50 | Non-recyclable (multi-material) | Retort pouches, pharma, oxygen-sensitive powders |
| PET / VMPET / PE (3-ply) | 0.5–2.0 | 1.0–3.0 | 25–40 | Limited (metallised layer disrupts PE stream) | Snacks, coffee, dry food |
| BOPP / EVOH / PE (3-ply) | 0.1–0.5 | 3.0–8.0 | 20–35 | Recyclable (all-polyolefin variant) | Dairy, fresh produce, sauces |
| Kraft paper / LDPE / Al foil / PE (4-ply) | < 0.05 | < 0.05 | 28–45 | Non-recyclable | Premium dry food, pet food |
| Mono-material PE / PE (BOPE) | 5.0–15.0 | 4.0–10.0 | 15–30 | Fully recyclable (PE stream) | Ambient snacks, e-commerce mailers |
| PET / SiOx-coated / PE (3-ply) | 0.3–1.5 | 0.5–2.0 | 25–40 | Better than foil (no metal layer) | Medical devices, nutraceuticals |
How to Select a Structure
- Match the barrier layer to the product’s failure mode: oxygen-sensitive products (oils, nuts, coffee) need EVOH or foil; moisture-sensitive products (powders, biscuits, salt) need low-WVTR layers such as metallised PET or foil.
- Nylon (BOPA) adds puncture resistance for hard, sharp products (pasta, bone-in meat, shell nuts) but is a poor moisture barrier — always pair it with a sealant and a moisture layer.
- For frozen products, barrier requirements drop sharply — a simple PE or BOPP/PE structure usually suffices and costs far less than a retort laminate.
Layer Architecture: Sealant, Barrier & Structural Layers
Every roll-stock structure is built from three functional layers. Understanding them lets you specify the minimum structure that meets spec — over-engineering adds cost and weight; under-specifying causes shelf-life failure.
| Layer | Common Materials | Function | Key Specification |
|---|---|---|---|
| Sealant (inner) | LDPE, LLDPE, mLLDPE, EVA, CPP, ionomer | Heat-seals the pack shut; hot-tack holds product weight before the seal cools | Seal initiation temperature, hot-tack strength, seal-window width |
| Barrier (middle) | Al foil, EVOH, VMPET, SiOx-coated PET, PVDC | Blocks oxygen, moisture, aroma, and UV | OTR / WVTR at defined RH and temperature |
| Structural (outer) | BOPET, BOPP, BOPA (nylon), paper, BOPE | Print surface, stiffness, puncture and tear resistance | Tensile strength, puncture resistance, COF, print adhesion |
A Note on Sealant Selection
- LLDPE / mLLDPE sealants give the widest heat-seal window and best hot-tack — the standard for high-speed VFFS.
- LDPE sealants cost less but have a narrower window and lower hot-tack — acceptable at slower speeds.
- Add EVA to lower seal initiation temperature; add ionomer (e.g. Surlyn®) for caustic or liquid fills that contaminate seals.
Machine & Process Compatibility
The film must be matched to the machine type — not just the product. Vertical (VFFS), horizontal (HFFS), flow-wrap, stick-pack, and thermoform-fill-seal lines each impose different mechanical demands on the web.
| Process | Typical Products | Key Film Demands | Recommended Structure |
|---|---|---|---|
| VFFS (vertical form-fill-seal) | Powders, granules, snacks, frozen, liquids | Low and stable COF, high hot-tack, tight gauge tolerance | BOPP/PE, PET/PE, PET/AL/PE, BOPP/EVOH/PE |
| HFFS (horizontal form-fill-seal) | Bars, biscuits, bakery, sachets | Stiffness for forming, low slip on former, precise registration | BOPP/PE, OPP/CPP, paper/PE |
| Flow-wrap (horizontal wrapper) | Confectionery, bakery, personal care | High gloss, low COF, cold-seal or heat-seal option | BOPP/PE, cast PP |
| Stick-pack / sachet | Powders, liquids, single-serve | Narrow web, high barrier, easy-tear notch | PET/AL/PE, PET/VMPET/PE |
| Thermoform-fill-seal (TFFS) | Medical devices, pharma, food trays | Deep-draw formability, high barrier, peelable seal | PVC/PE, PET/PE, APET/PE |
Regulatory & Compliance Matrix
Food-contact and export compliance is non-negotiable. The matrix below maps the frameworks we qualify against. Request the specific declaration of compliance (DoC) for your target market at the RFQ stage.
| Regulation / Standard | Region | What It Governs | What We Provide |
|---|---|---|---|
| FDA 21 CFR 177.1520 / 177.1390 | USA | Olefin polymers and laminate adhesives in food contact | FDA-compliant resins and adhesives, migration data |
| EU 10/2011 (EC 1935/2004) | European Union | Plastics in food contact, overall migration limits (OML 10 mg/dm²) | DoC plus SML test reports per structure |
| GB 4806.7 & GB 9685 | China | Food-contact plastics and additives | GB-compliant materials, migration certificates |
| REACH (EC 1907/2006) | EU | SVHC and restricted substances in articles | REACH SVHC declaration |
| California Prop 65 | USA (CA) | Listed chemicals (phthalates, lead, BPA) | Prop 65-safe ink and substrate options |
| BRCGS Packaging (Issue 6) | Global | Packaging-materials food-safety management | Hygienic production, HACCP-aligned controls |
| ISO 22000 / ISO 9001 | Global | Food-safety and quality management systems | Certified QMS, full lot traceability |
| EN 13432 / PPWR (EU 2025/40) | EU | Compostability / packaging recyclability and EPR | Mono-material options, recycled-content roadmaps |
Sustainability & Recyclable Structures
The EU PPWR and rising extended-producer-responsibility (EPR) fees are forcing a shift from multi-material laminates to recyclable mono-material structures. The engineering challenge: mono-PE films historically sacrifice barrier and machinability. The table below shows the trade-offs and where MDO/BOPE and SiOx coatings now close the gap.
| Structure | Barrier Level | Machinability on FFS | Recyclability | Best Fit |
|---|---|---|---|---|
| Multi-material (PET/AL/PE) | Excellent (< 0.01 OTR) | Excellent | Not recyclable | Long shelf life, oxygen-critical |
| Metallised PET/PE | Good (0.5–2.0 OTR) | Good | Limited | Snacks, dry food |
| Mono-PE with SiOx / AlOx coating | Good (0.3–1.5 OTR) | Good | Fully recyclable (PE stream) | PPWR-compliant barrier applications |
| Mono-PE (BOPE/PE) | Moderate (5–15 OTR) | Moderate (needs tight COF control) | Fully recyclable | Ambient snacks, mailers |
| Paper-based (paper/PE) | Low–moderate | Moderate | Partially recyclable | Dry goods, bakery, premium |
| PCR-content PE film | Moderate | Moderate (gauge consistency varies) | Recyclable | Non-food or secondary packaging |
Total Cost of Ownership: Why the Cheapest Film Is Rarely the Cheapest Line
Procurement teams often optimise film price per kg in isolation. That metric ignores the dominant cost driver on an automated line: machine efficiency (OEE). A film that runs 5% slower or causes 2% more rejects can erase ten times its purchase-price saving.
| Cost / Performance Metric | Low-Cost Film | Engineered Roll Stock |
|---|---|---|
| Film price (per kg) | Lowest | Typically 3–8% higher |
| Machine speed (OEE) | Reduced by COF and tension variation | Full rated speed, stable web tension |
| Defect / reject rate | Higher (seal failures, misregistration) | Low — controlled COF and seal window |
| Downtime (roll changes, jams) | More frequent | Fewer; longer roll runs |
| Product waste and give-away | Higher (over-pack, leakers) | Lower |
| Shelf life / returns | Barrier drift → early spoilage | Stable barrier → longer shelf life |
| Net cost per 1,000 packs | Often higher | Lower despite higher film price |
Rule of thumb from high-volume converters: a 5% film-cost saving that costs 1% of line OEE is a net loss at any meaningful volume. Evaluate film on cost per 1,000 finished packs, not cost per kg.
Applications by Industry
- Food & beverage — snacks, coffee, confectionery, frozen, dairy, pet food, sauces, and powders; the largest and most barrier-sensitive segment.
- Pharmaceuticals & nutraceuticals — sachets, stick packs, and medical-device pouches requiring validated barrier and clean-room conversion.
- Personal care & cosmetics — single-dose sachets and sample packs with high-gloss, retail-quality print.
- Home care & chemicals — detergents, cleaning agents, and agrochemicals needing chemical-resistant sealants.
- Industrial & hardware — fasteners, components, and electronics with optional ESD-safe and anti-static films.
Customization Options
- Material and structure — any sealant / barrier / structural combination, from monolayer PE to 4-ply retort laminates.
- Thickness (gauge) — typically 20–150 µm, with tight gauge tolerance (±3% or better) for high-speed consistency.
- Width and roll format — slit to your exact machine width; 76 mm or 152 mm cores; unwind direction matched to your machine.
- Printing — gravure or flexo up to 10 colors; matte or gloss; spot UV; registered cold-seal or heat-seal patterns.
- Functional add-ons — easy-tear notches, laser scoring, one-way degassing valves, anti-fog, ESD-safe, high/low-slip surfaces, UV barrier.
- Finishes — clear, white, metallised, kraft-look, and pearlescent.
Quality Control & Test Methodology
Every production lot is tested against the specification you approve. Below is the standard test panel — request the full certificate of analysis (CoA) per lot.
| Test | Standard | What It Verifies | Typical Specification |
|---|---|---|---|
| Coefficient of friction (COF) | ASTM D1894 / ISO 8295 | Film-to-metal and film-to-film slip for web tracking | Kinetic 0.12–0.25 (film-to-metal) |
| Heat seal strength | ASTM F88 | Seal integrity and peel strength | ≥ 20 N/15 mm (structure-dependent) |
| Hot tack | ASTM F1921 | Seal strength while still hot (product weight before cooling) | ≥ 3 N/15 mm at seal temperature |
| OTR (oxygen transmission) | ASTM D3985 | Oxygen barrier | Per structure (see §2) |
| WVTR (moisture transmission) | ASTM F1249 | Water-vapour barrier | Per structure (see §2) |
| Tensile strength and elongation | ASTM D882 | Web strength under tension | Structure-dependent |
| Puncture resistance | ASTM F1306 / D5748 | Resistance to sharp product | Structure-dependent |
| Gauge / thickness uniformity | ASTM D6988 | Consistent thickness for tension control | ±3% of nominal |
| Dyne level (surface energy) | ASTM D2578 | Print and lamination adhesion readiness | ≥ 38 dyn/cm (print side) |
| Dart drop impact | ASTM D1709 | Impact toughness | Structure-dependent |
Failure Modes & Prevention
This is the section most suppliers don’t publish. Each failure mode below is one we have been asked to diagnose on a customer’s line — and the prevention we engineer into the film specification.
| Failure Mode | Typical Root Cause | How It’s Detected | Prevention (Engineered Into Spec) |
|---|---|---|---|
| Film breakage / web snap | Excessive COF on forming collar, tension spike, gauge variation | Line stop, material waste | Controlled COF 0.12–0.25, ±3% gauge, high-tensile web |
| Seal leakage / weak seal | Insufficient seal temperature or dwell; contaminated sealant | Leak test, drop test | Wide heat-seal window, high hot-tack sealant |
| Seal burn-through | Temperature overshoot beyond seal window | Visual; weak seal at edges | Wide seal window (low seal initiation, high burn-through resistance) |
| Misregistration / drift | Unstable COF or web tension, off-spec unwind | Print misalignment | Consistent COF, controlled unwind, tension-stable web |
| Static cling / film sticking | High static charge on film | Jams, mis-feeds | Anti-static / slip additives, controlled humidity |
| Barrier failure / short shelf life | Pinholing in foil or metallised layer; flex-cracking | Shelf-life test, OTR re-test after flex | Pinhole-free foil spec, flex-crack-resistant metallisation, barrier-degradation allowance |
| Curling / poor flatness | Unbalanced layer shrinkage; moisture in paper ply | Forming defects | Balanced structure, controlled-humidity storage |
| Delamination | Insufficient lamination bond; adhesive failure | T-peel test | Bond strength ≥ 2.5 N/15 mm (ASTM F904); solvent-based PU adhesive for foil/EVOH |
MOQ, Pricing Factors & Lead Time
Pricing is driven by five variables, in rough order of impact. Understand these and you can quote accurately and compare suppliers fairly.
| Pricing Factor | Impact | How to Optimise |
|---|---|---|
| Film structure (materials) | Foil / EVOH / SiOx raise cost; monolayer PE is lowest | Spec the minimum barrier that meets shelf life |
| Order volume | Higher volume lowers per-kg cost (spreads plate/setup costs) | Consolidate orders; forecast quarterly |
| Printing method (gravure vs flexo) | Gravure cylinders add a one-time cost per design; flexo has lower setup | Flexo for short runs; gravure for long runs / fine art |
| Number of colors | Each color adds cylinder/plate and ink cost | Limit to brand-essential colors |
| Special requirements | Retort, cold-seal, special coatings, tight gauge all add cost | Confirm the spec is truly required |
Typical parameters: MOQ from ~200 kg on printed structures (rotogravure); 7–15 working days on repeat structures; free stock samples for machine trials. New tooling (gravure cylinders) adds 5–10 days plus a one-time cylinder fee.
Production Process — From Resin to Finished Roll
- Structure and artwork engineering — we confirm barrier targets, seal window, COF, gauge, and print file against your machine specification.
- Raw-material intake and QC — resin, foil, ink, and adhesive lots are quarantined and tested before release.
- Printing — gravure or flexo up to 10 colors with in-line color control and registration cameras.
- Lamination — dry-bond or solvent-free lamination; extrusion lamination for selected structures.
- Slitting — to your exact roll width and core size, with tension-controlled winding.
- Curing and conditioning — solvent lamination cures to full bond strength before slitting and dispatch.
- Final QC and CoA — each lot tested (COF, seal, barrier, gauge) and shipped with a certificate of analysis.
- Packaging and dispatch — rolls wrapped, labelled, and palletised for export.
Supplier Evaluation Checklist — 15 Points for Procurement
Use this when shortlisting roll-stock suppliers. A supplier who can answer all 15 with data — not assurances — is one you can run at high speed without supervision.
- Can they provide quantified OTR and WVTR per structure, with test conditions stated?
- Do they control COF and publish the target range (film-to-metal and film-to-film)?
- Do they guarantee gauge uniformity (±3% or tighter) and provide per-lot gauge charts?
- Do they test heat-seal strength and hot tack — not just seal ‘yes/no’?
- Can they run a sample-roll trial on your exact machine before bulk order?
- Are they certified to ISO 9001 (and BRCGS Packaging / ISO 22000 for food)?
- Do they hold FDA / EU 10/2011 / GB declarations of compliance for the specific structure you are buying?
- Do they offer recyclable (mono-material) options and have PPWR / EPR data?
- Is printing done in-house (gravure/flexo) with color management and registration QC?
- What is their real lead time and MOQ — and can they hold safety stock or run VMI?
- Do they provide lot-level certificates of analysis (CoA) with every shipment?
- What is their defect/reject policy — credit, replacement, or rework?
- Can they support film trials for new product launches and line changes?
- Do they have export experience to your market and compliant export documentation?
- Are they audited for social and environmental compliance (BSCI, ISO 14001)?
Market Intelligence for Decision-Makers
The global flexible film market was valued at roughly USD 37.6 billion in 2024 and is forecast to reach about USD 64.9 billion by 2035, growing at ~5.1% CAGR. Within the broader flexible packaging market (USD ~300 billion in 2025), plastic films are the largest material segment (~53% share), and Asia-Pacific — led by China — is both the largest and fastest-growing region.
Three structural trends are reshaping roll-stock procurement, and are worth planning for now:
- Mono-material transition — PPWR and EPR fees are pulling buyers from multi-layer laminates to recyclable mono-PE and coated mono-materials; early adopters are locking in compliant structures before fees escalate.
- Sustainability-mandated redesign — brands are under retailer pressure to cut weight and add recycled content, driving demand for thinner, stronger, and PCR-containing films.
- Resin-price volatility — PE/PP feedstock swings (naphtha/ethane) make multi-quarter contracting and VMI programs more attractive than spot buying.
For a procurement leader, the strategic question is not ‘which supplier is cheapest this quarter’ but ‘which supplier can keep my line running at full OEE across a material transition.’ That is the standard this page is written to.
Frequently Asked Questions
What is the minimum order quantity (MOQ) for automatic packaging film?
Printed structures typically start around 200 kg (rotogravure); some monolayer or clear structures can start lower. Flexo-printed runs have lower setup costs and are better for short runs. Tell us your machine width and annual volume and we will recommend the printing method that minimises your total cost.
Can I get a sample roll to test on my VFFS/HFFS machine before ordering?
Yes — and we strongly recommend it. We supply free stock sample rolls (with printing on request) so you can validate COF, seal window, and machinability on your exact machine and product before committing. It is the single cheapest way to avoid a costly misfit.
How do I know which film structure my product needs?
Send us three data points — your product and its failure mode (oxygen-sensitive, moisture-sensitive, sharp, frozen), your target shelf life, and your machine type (VFFS/HFFS/stick-pack). We will specify the minimum barrier structure that meets your shelf life and machine demands, backed by OTR/WVTR data.
What is COF and why does it matter for automatic packaging?
COF (coefficient of friction) controls how the film slides over the forming collar and through rollers. Too high and the web jams or tears; too low and it slips and misregisters. For VFFS lines the target is typically kinetic COF of 0.12–0.25 film-to-metal, tested to ASTM D1894 or ISO 8295. We control COF per lot and report it on the CoA.
Do your films meet food-contact and export regulations?
Yes. We supply structures compliant with FDA 21 CFR, EU 10/2011 (with declaration of compliance), China GB 4806.7 / GB 9685, and REACH, with Prop 65-safe ink options. Specify your destination market at RFQ and we provide the matching DoC and migration test reports.
Can you supply recyclable or mono-material films?
Yes — we offer mono-PE (BOPE) and SiOx/AlOx-coated mono-material structures for PPWR compliance, plus PCR-content options for non-food applications. Barrier levels are lower than foil laminates, so we will help you confirm the trade-off against your shelf-life requirement.
What lead time should I expect?
Repeat structures ship in 7–15 working days. New structures with new gravure cylinders add roughly 5–10 days plus a one-time cylinder fee. For recurring high-volume programs we can hold safety stock or run a VMI program to cut lead time to a few days.
What information do you need for an accurate quote?
Machine type and jaw/forming dimensions, film width, product and fill weight, required barrier (or target shelf life), printing (colors and file), annual volume, and destination market. With those we return a structure recommendation and quote within 24 hours.
Key Takeaways
- Automatic packaging film is a consumable that controls line speed, seal integrity, and barrier — spec it on OEE and cost per pack, not price per kg.
- The three machine-critical specs are COF (0.12–0.25 kinetic, film-to-metal), a wide heat-seal window with high hot-tack, and tight gauge uniformity (±3%).
- Match the barrier layer to the product’s failure mode, and confirm OTR/WVTR test conditions before comparing suppliers.
- A 5% film-cost saving that costs 1% of OEE is a net loss — TCO, not unit price, is the correct procurement metric.
- Get a sample roll and run it on your machine before bulk ordering — it is the cheapest insurance in packaging.
Spec Your Film With an Engineer, Not a Catalogue
Tell us your machine type, product, and barrier target, and we will return a quantified structure recommendation — with OTR/WVTR, COF, and seal-window data — plus a sample roll for on-line trial. Reach us at sales@packagingcustom.cn or use the contact form.
You Also May Like
Ready to Improve Your Packaging Supply Chain?
Whether you are looking for a new packaging supplier, a backup manufacturer, or a trusted sourcing partner, We are ready to support your business.