Custom Coffee Bags
— Engineered Barrier Packaging for Fresh-Roasted Coffee
A custom coffee bag is a high-barrier flexible pouch engineered to hold freshly roasted coffee — whole bean or ground — that continuously off-gasses CO2 after roasting while blocking oxygen, moisture, UV light and aroma loss. Built for roasters, packaging engineers and procurement teams who specify coffee packaging as an engineering component, not a commodity.
What you can expect from our factory
- ISO 9001:2015 quality system with food-contact material compliance (FDA 21 CFR 177.1520, EU 10/2011, GB 4806, REACH, Prop 65)
- Quantified barrier data — OTR in cc/m²/day and WVTR in g/m²/day per film structure, with the exact test conditions stated
- One-way degassing valves (with or without filter), resealable zippers, tin-ties, tear notches and clear windows, all in-house
- Formats: flat-bottom (box), quad-seal, side-gusset, stand-up and pillow/brick, from 100 g to 5 lb fill weight
- Free pre-production samples in 3–5 days; MOQ from 1,000 pieces; production lead time 7–15 days
Anatomy of a Coffee Bag: Every Component, Specified
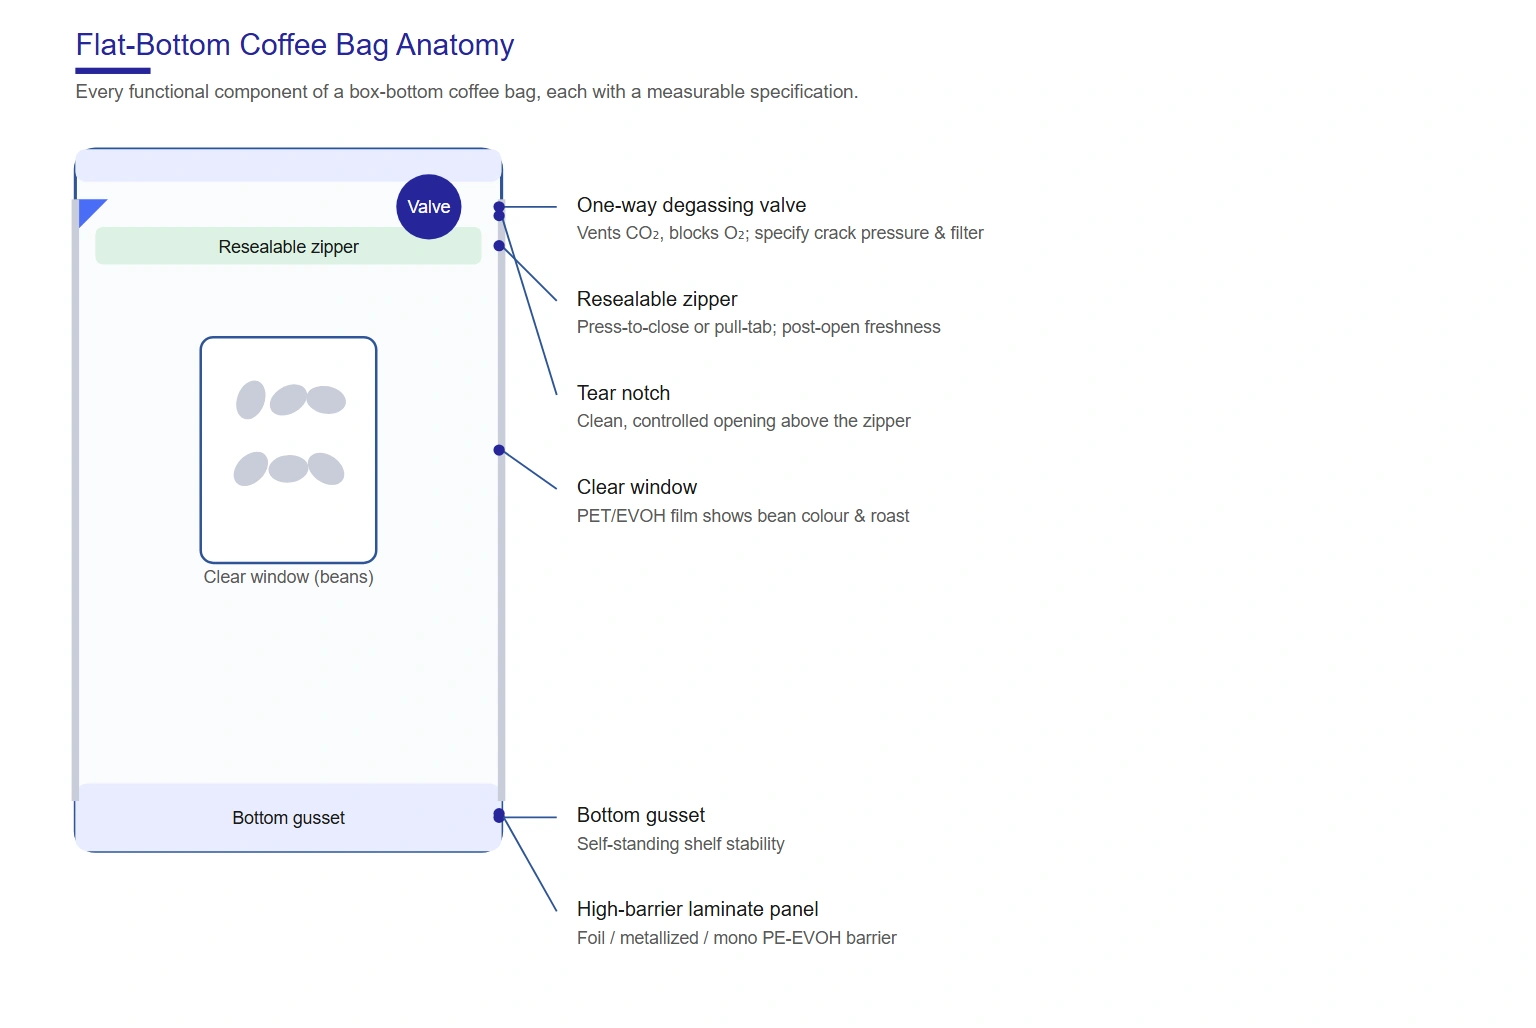
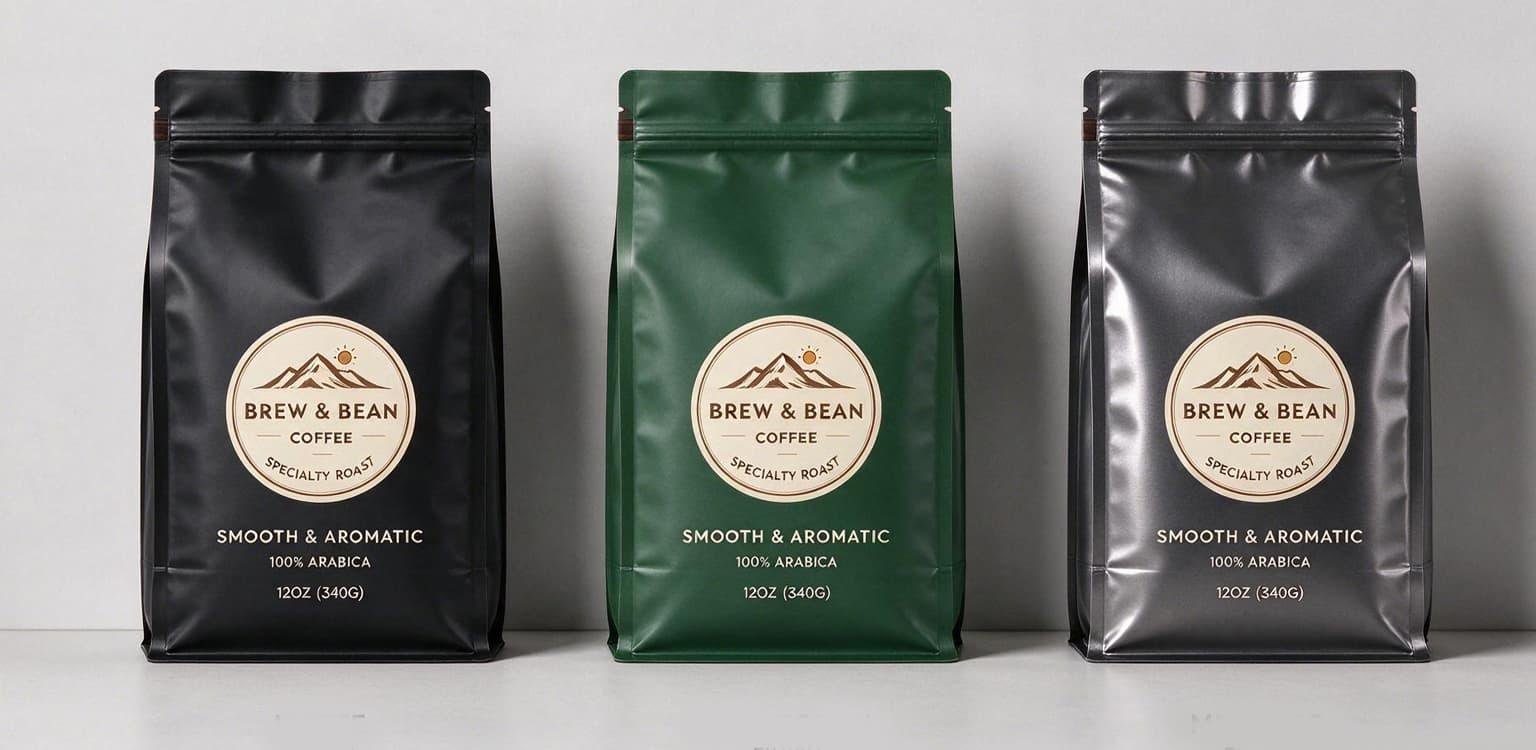
A coffee bag is a system of interacting components, and each one has a measurable specification that affects shelf life and fill-line behaviour. The diagram below labels a flat-bottom (box) coffee bag; the table that follows gives the specification you should be able to ask any supplier to quantify.
| Component | Function | Key specification to request |
|---|---|---|
| One-way degassing valve | Vents CO2 from the roast; blocks O2 ingress | Crack (opening) pressure, filter vs. no-filter, body material, heat-seal temperature |
| Front / back panels | Branding surface + primary barrier | Laminate structure, OTR/WVTR, print finish (matte/gloss/metallic) |
| Bottom gusset | Self-standing stability on shelf | Gusset depth (mm), crease quality, fold geometry |
| Resealable zipper | Freshness after first open | Press-to-close vs. pull-tab, opening force, re-close cycle life |
| Tear notch | Clean, controlled opening | Position, depth, laser vs. mechanical notch |
| Side / top seals | Containment and integrity | Seal width, seal strength (N/15 mm, ASTM F88), burst resistance |
| Clear window | Product visibility | Window film (PET/EVOH), clarity, seal compatibility |
| Tin-tie (optional) | Roll-top reseal for gusset bags | Wire gauge, tape adhesion, fold endurance |
Film Structure & Barrier Engineering: The Numbers That Matter
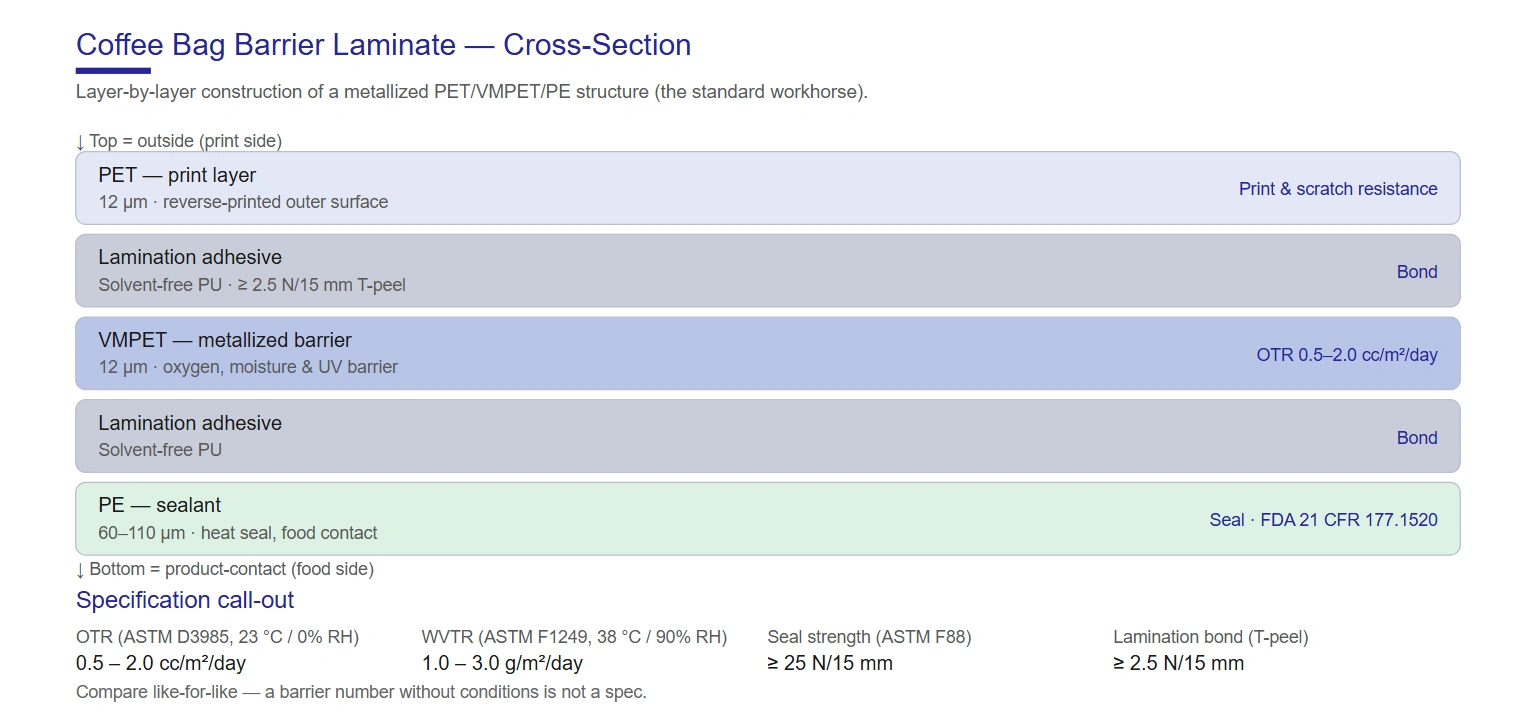
Coffee is among the most barrier-demanding foods in flexible packaging. Oxygen drives staling and rancidity of the coffee oils; moisture migrates in and dulls the cup; UV degrades aromatics. The table below gives the oxygen transmission rate (OTR) and water vapour transmission rate (WVTR) for the laminate structures we run, with the test conditions stated — because a barrier number without conditions is meaningless.
| Film structure | OTR (cc/m²/day) | WVTR (g/m²/day) | Recyclability | Typical use |
|---|---|---|---|---|
| PET / Al foil / PE (3-ply) | < 0.01 | < 0.01 | Non-recyclable | Premium & high-oleicity beans, longest shelf life |
| Kraft / LDPE / Al / PE (4-ply) | < 0.05 | < 0.05 | Non-recyclable | Kraft-look retail bags, whole bean |
| MAT-OPP / VMPET / PE (3-ply) | 0.5 – 2.0 | 1.0 – 3.0 | Limited | Standard metallized coffee bag — workhorse structure |
| Kraft / VMPET / PE (3-ply) | 0.5 – 2.0 | 1.0 – 3.0 | Limited | Kraft exterior, metallized barrier |
| PE / EVOH / PE (mono, recyclable) | 0.1 – 0.5 | 3.0 – 8.0 | Recyclable (all-polyolefin) | Mono-material / recyclable programs |
| Kraft paper / PLA / PLA (compostable) | 5.0 – 15.0 | 4.0 – 10.0 | Compostable (industrial) | Compostable coffee bags |
Conditions: OTR per ASTM D3985 @ 23 °C / 0% RH; WVTR per ASTM F1249 @ 38 °C / 90% RH. The same film read at 23 °C / 50% RH can report up to 3× higher OTR — always compare like-for-like.
How to select a structure (engineer's checklist)
- Shelf-life target first. ≤ 6 months and cost-sensitive → metallized (VMPET). ≥ 12 months, high-oleic or premium → foil. Recyclability mandate → mono PE/EVOH and accept a shorter shelf life.
- Add a 10% barrier-degradation allowance for metallized structures — flex-cracking during forming degrades VMPET barrier.
- Match the sealant to the fill line. LLDPE sealant for hot-tack and speed; a wide seal window (low initiation + high burn-through resistance) buys line speed and fewer rejects.
- State the test conditions on every supplier spec. OTR/WVTR quoted without temperature and RH is a marketing number, not an engineering number.
One-Way Degassing Valve Engineering
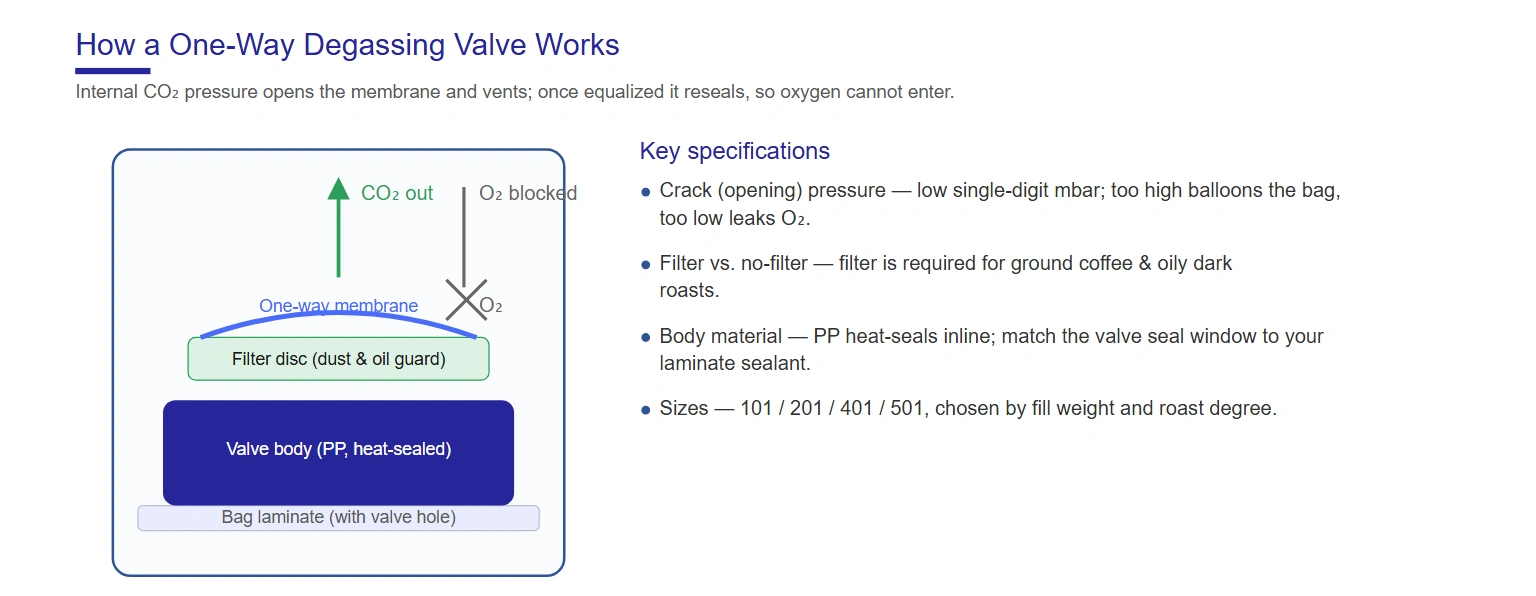
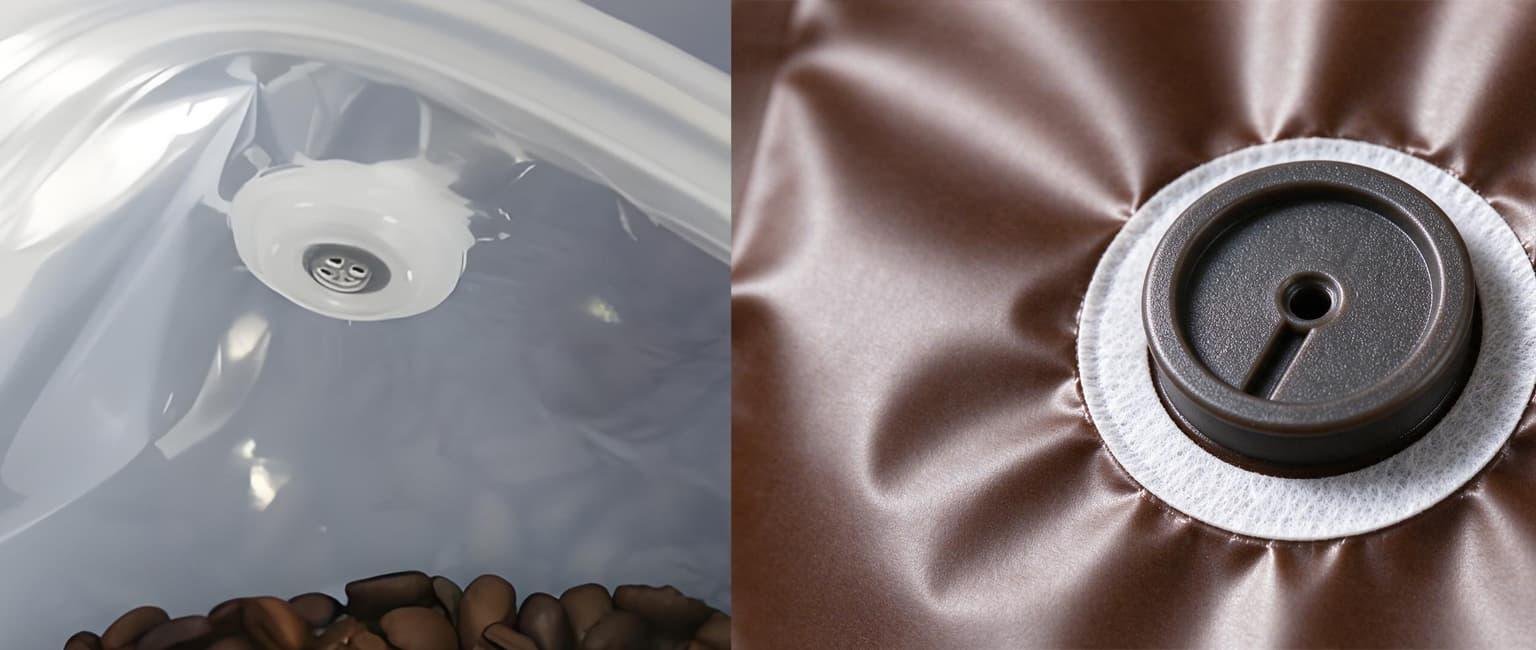
The degassing valve is the single most misunderstood component in coffee packaging. It is a one-way pressure-relief device: it opens when internal CO2 pressure exceeds a set crack pressure and closes when the pressure equalizes, so roasted gas escapes while ambient air (20.9% O2) stays out. Valve size codes follow the industry standard — 101, 201, 401 and 501 — and the choice is driven by fill weight, roast degree and bag format.
| Valve size code | Approx. body diameter | Typical application | Notes |
|---|---|---|---|
| 101 | ~16 mm | Small retail bags, ≤ 250 g | Lower profile, lower flow rate |
| 201 | ~20 mm | 250 g – 1 kg retail (most common) | Industry default; with or without filter |
| 401 | ~24 mm | 1 kg – 2 lb formats | Higher flow for larger fills |
| 501 | ~27 mm | 5 lb / foodservice / bulk | Maximum flow, high degas volume |
- Crack (opening) pressure — request it. Typical coffee valves open in the low single-digit mbar range; too high a crack pressure lets the bag balloon, too low compromises the O2 barrier.
- Filter vs. no-filter. A filter (non-woven PP/PET disc) stops coffee dust and oil from fouling the membrane — required for ground coffee and oily dark roasts.
- Body material. PP valve bodies heat-seal directly into the laminate; verify the valve’s seal temperature window against your laminate’s sealant.
- Application method. In-line heat-seal application on the pouch line is standard; self-adhesive valves suit retrofit/tin-tie programs.
Coffee Degassing & Freshness Science
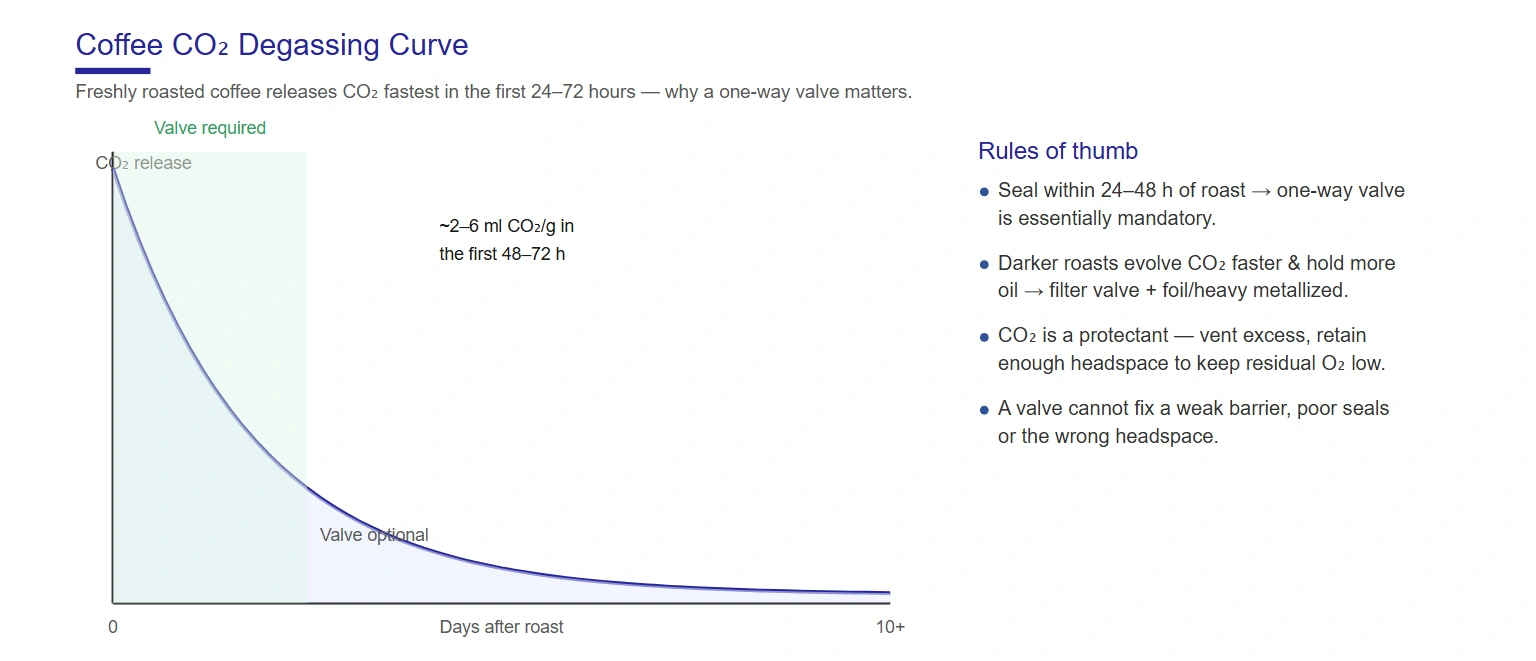
Roasting drives CO2 deep into the bean cell structure; that gas escapes over days, a process called degassing. Freshly roasted whole beans typically evolve on the order of 2–6 ml CO2 per gram in the first 48–72 hours, with the steepest release in the first 24 hours — which is exactly why a sealed bag without a valve balloons and can burst. This is not a cosmetic issue: trapped CO2 is also what displaces oxygen, so a valve that vents too early lets freshness out with the gas.
- Rule of thumb: if you seal coffee within 24–48 hours of roast, a one-way valve is essentially mandatory. Beyond ~5–7 days post-roast (or for pre-ground, nitrogen-flushed brick packs), the valve is optional.
- Roast degree matters. Darker roasts evolve CO2 faster and hold more oil on the surface — pair dark roasts with a filter valve and a foil or heavy metallized barrier.
- CO2 is a protectant, not a problem. The ideal bag vents excess pressure while retaining enough CO2 headspace to keep residual oxygen low.
- Valve does not fix a weak barrier. A valve cannot correct a poor seal, the wrong headspace, or unsuitable packing timing — specify barrier and valve together as one system.
Coffee Bag Formats & Fill Weights
| Format | Structure | Best for | Shelf presence | Relative cost |
|---|---|---|---|---|
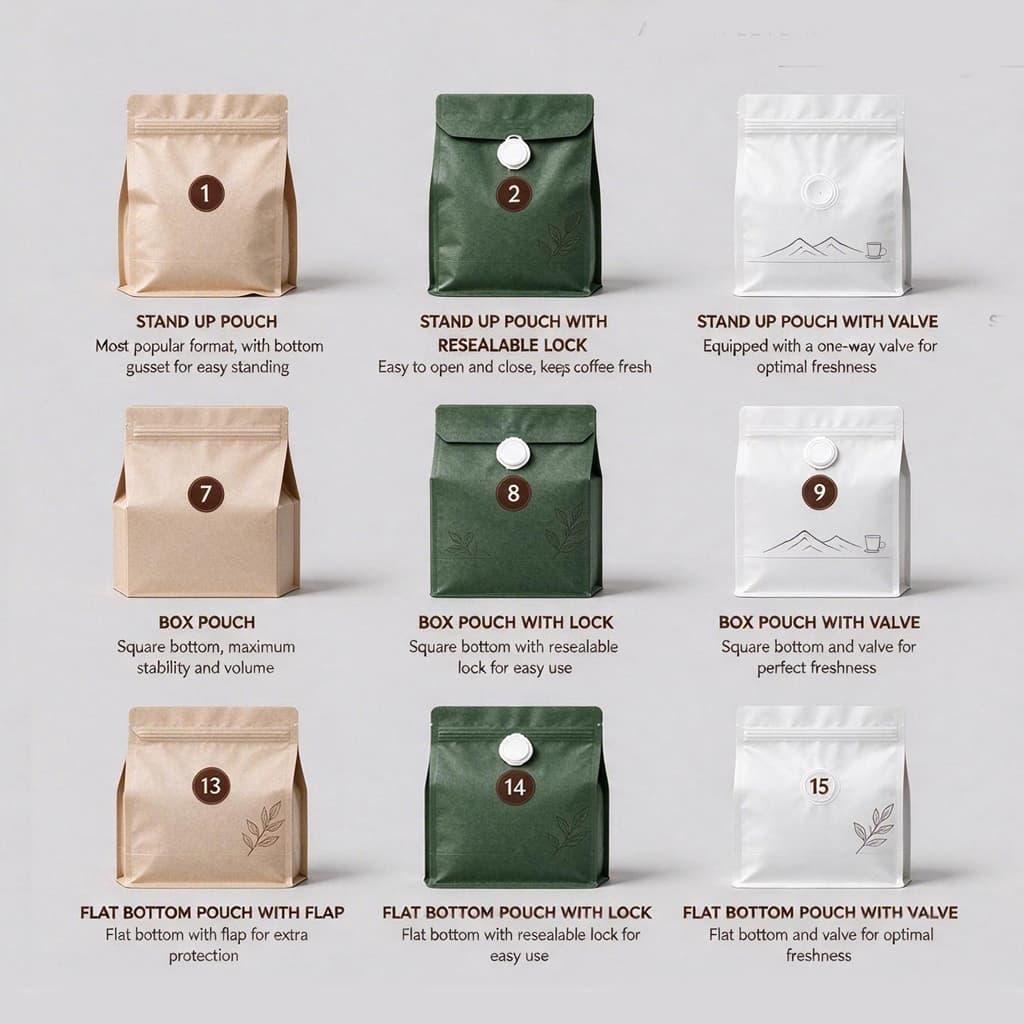
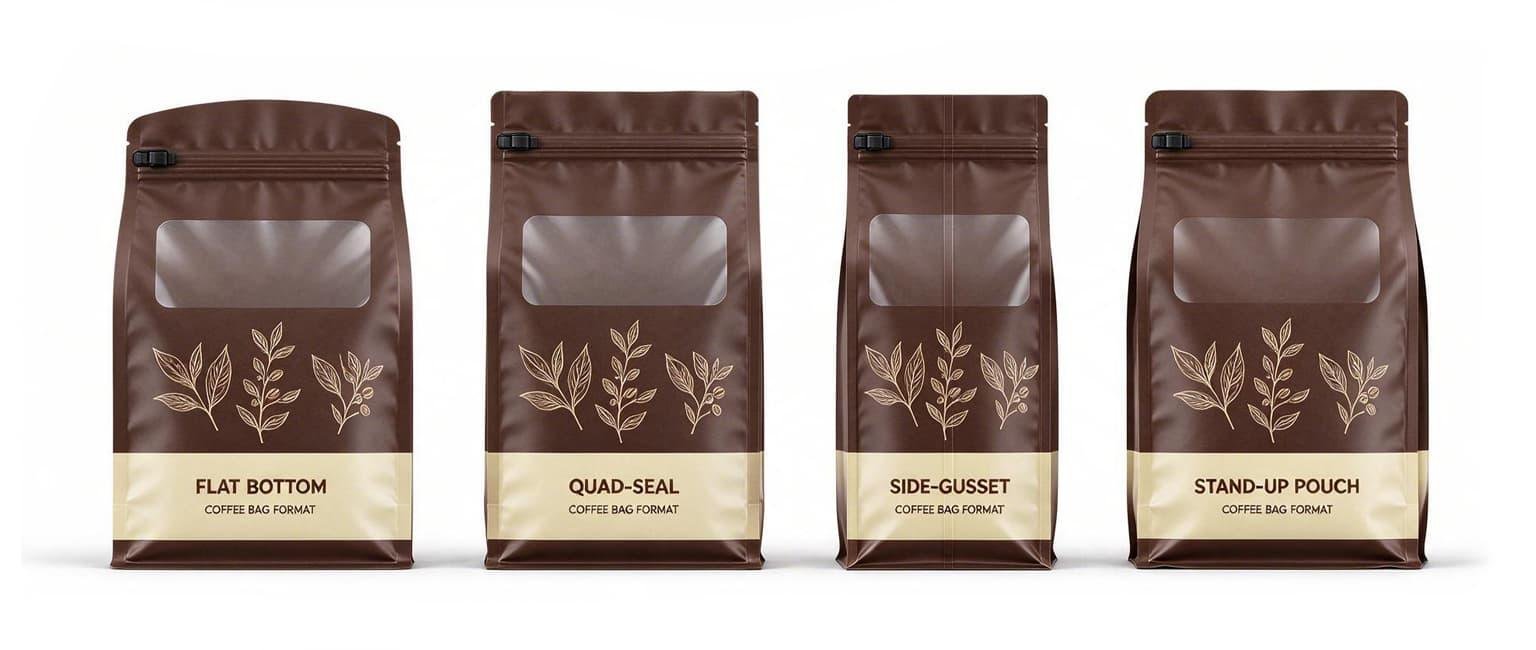
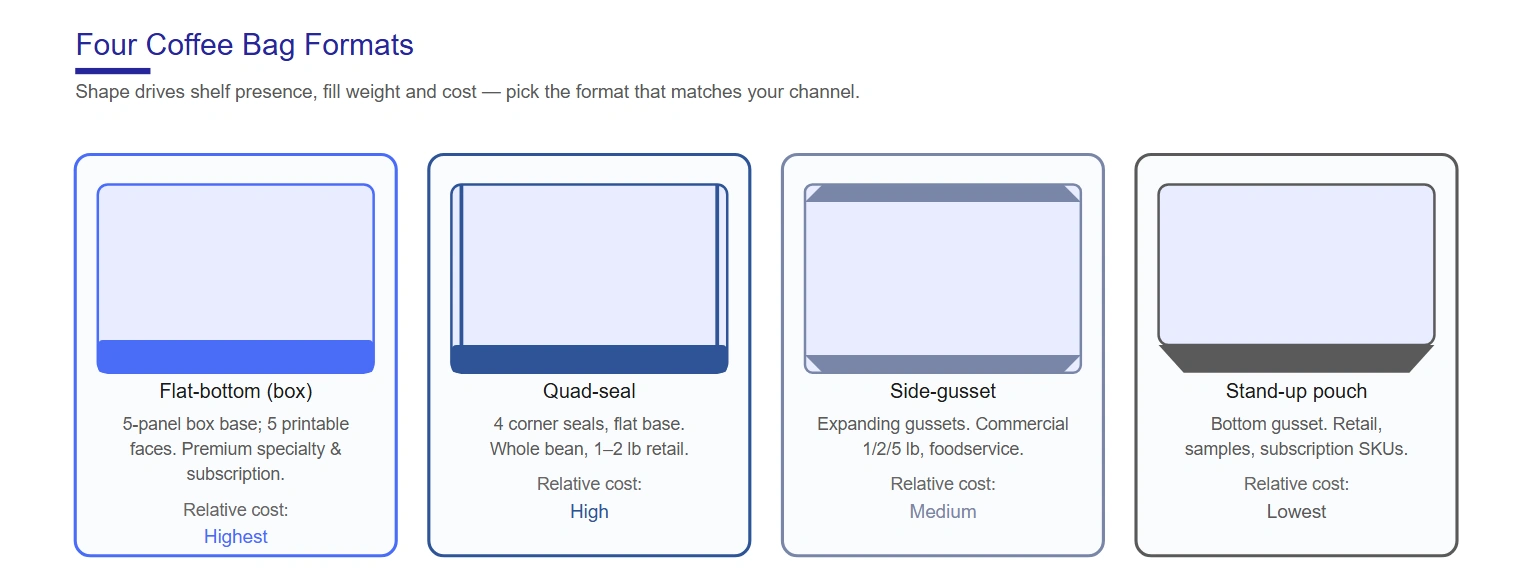
| Flat-bottom (box / 8-side seal) | 5-panel box base | Premium specialty & third-wave brands, subscription | Excellent — self-standing, 5 printable faces | Highest |
| Quad-seal (4-corner) | 4 corner seals, flat base | Whole bean, 1–2 lb retail | Very good — box-like | High |
| Side-gusset | Expanding side gussets | Commercial roasters, 1/2/5 lb, foodservice | Good — traditional | Medium |
| Stand-up pouch (Doypack) | Bottom gusset | Retail, samples, subscription SKUs | Good — familiar, compact | Lowest |
| Pillow / brick | Fin-seal, N2-flushed | High-volume ground coffee | Flat, stackable | Lowest |
| Fill weight | Format (typical) | Reference dimensions (W × H + gusset) |
|---|---|---|
| 100 g / 4 oz | Stand-up pouch | 130 × 200 + 70 mm |
| 250 g / 8 oz | Flat-bottom or stand-up | 160 × 220 + 70 mm (SUP) / 240 × 90 × 70 mm (box) |
| 500 g / 1 lb | Flat-bottom or quad-seal | 200 × 265 + 120 mm |
| 1 kg / 2 lb | Flat-bottom or side-gusset | 235 × 300 + 110 mm / 320 × 135 × 95 mm (box) |
| 5 lb / 2.3 kg | Side-gusset (foodservice) | Custom — sized to density |
Dimensions are reference points; the final size is calculated from your coffee’s bulk density (typically 0.32–0.42 g/ml for whole bean, 0.40–0.55 g/ml for ground) plus headspace for the valve and seal.
Closures & Fitments
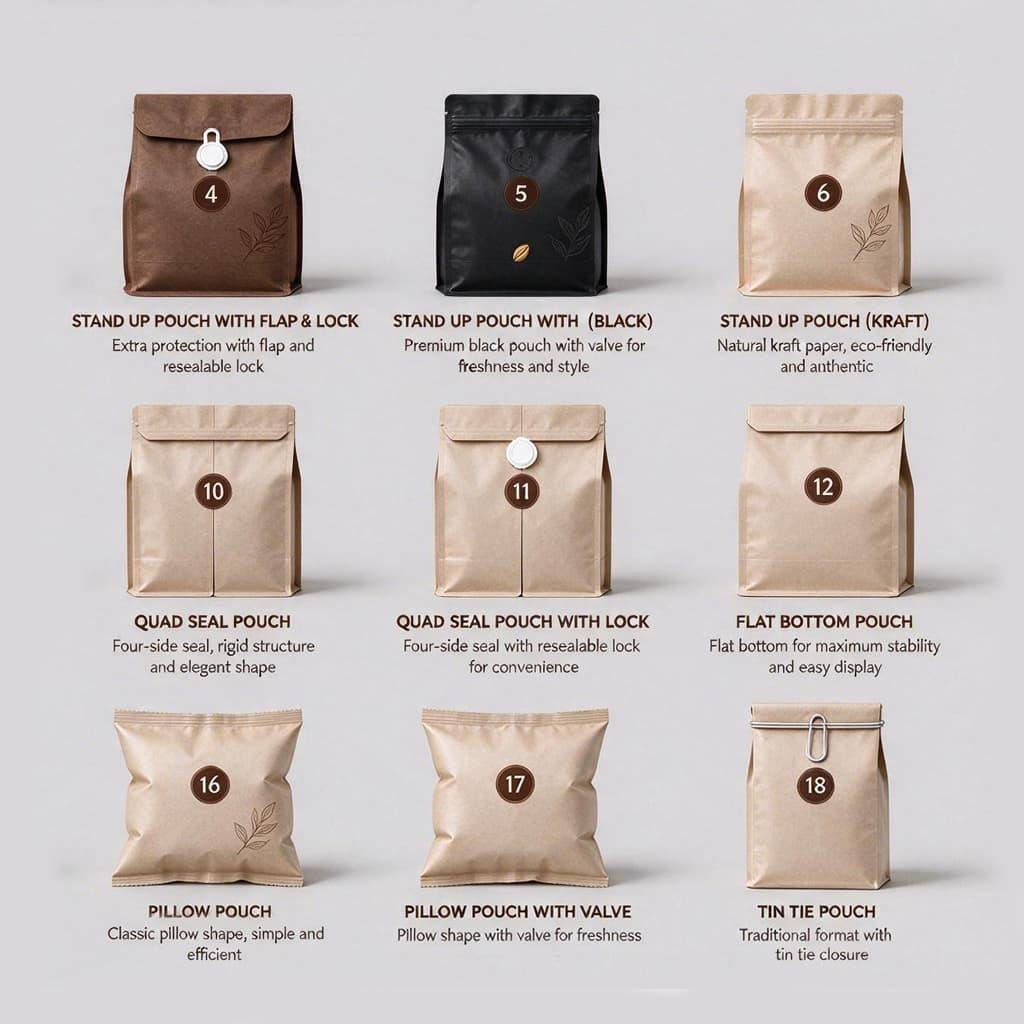
- Press-to-close zipper — standard reseal, lowest cost, suits stand-up and flat-bottom retail.
- Pull-tab (EZ-pull) zipper — easier open for consumers, wider mouth, preferred for flat-bottom premium bags.
- Tin-tie roll-top — the classic gusset-bag reseal; pair with an easy-peel interior liner for a tight seal.
- Tear notch — laser or mechanical, positioned above the zipper so the zipper survives the first open.
- Hang hole — for retail pegs and subscription mailers.
- Clear window — PET or EVOH window film heat-sealed into the panel to show bean colour and roast.
Filling, Nitrogen Flushing & MAP Compatibility
Your bag must match your packing line, not fight it. The table below maps common coffee packing processes to the structure and features required.
| Process | What it demands of the bag | Recommended structure / feature |
|---|---|---|
| Nitrogen flushing (MAP) | Low residual O2 (< 1–2%) requires a tight barrier to hold the flush | Foil or heavy metallized; sealed valve |
| Hot-fill / warm seal | Wide heat-seal window, high hot-tack for line speed | LLDPE sealant, optimized seal-layer gauge |
| Valve-applied inline | Valve heat-seal must survive downstream seals | PP valve, matched seal-temperature window |
| High-speed VFFS (brick/pillow) | Low & consistent COF (0.12–0.25), clean hot-tack | Film with controlled slip additive |
| Hand/bench packing (micro-roasters) | Easy-open, forgiving seals | Tin-tie or zipper, standard sealant |
Regulatory & Compliance Matrix
| Standard / regulation | Scope | What it covers for coffee bags |
|---|---|---|
| FDA 21 CFR 177.1520 / 177.1390 | USA | Olefin polymers & laminate adhesives for food contact |
| EU 10/2011 (EC 1935/2004) | EU | Plastics food-contact; overall migration limit 10 mg/dm² |
| GB 4806.7 / GB 9685 | China | Food-contact plastics & additives |
| REACH (EC 1907/2006) | EU | SVHC declaration on materials & inks |
| California Prop 65 | USA (CA) | Phthalates, lead, BPA limits |
| BRCGS Packaging (Issue 6) | Global | Packaging food-safety management system |
| ISO 22000 / ISO 9001 | Global | Food-safety & quality management |
| EN 13432 / OK Compost / BPI | EU / US | Industrial compostability of paper-PLA structures |
| RecyClass / APR design guidance | EU / US | Recyclability of mono-material structures |
We supply a Declaration of Compliance (DoC) and migration-test certificates for every shipped structure. Ask for the DoC — a supplier that cannot produce one for a food-contact coffee bag has not done the compliance work.
Sustainability & Recyclable / Compostable Structures
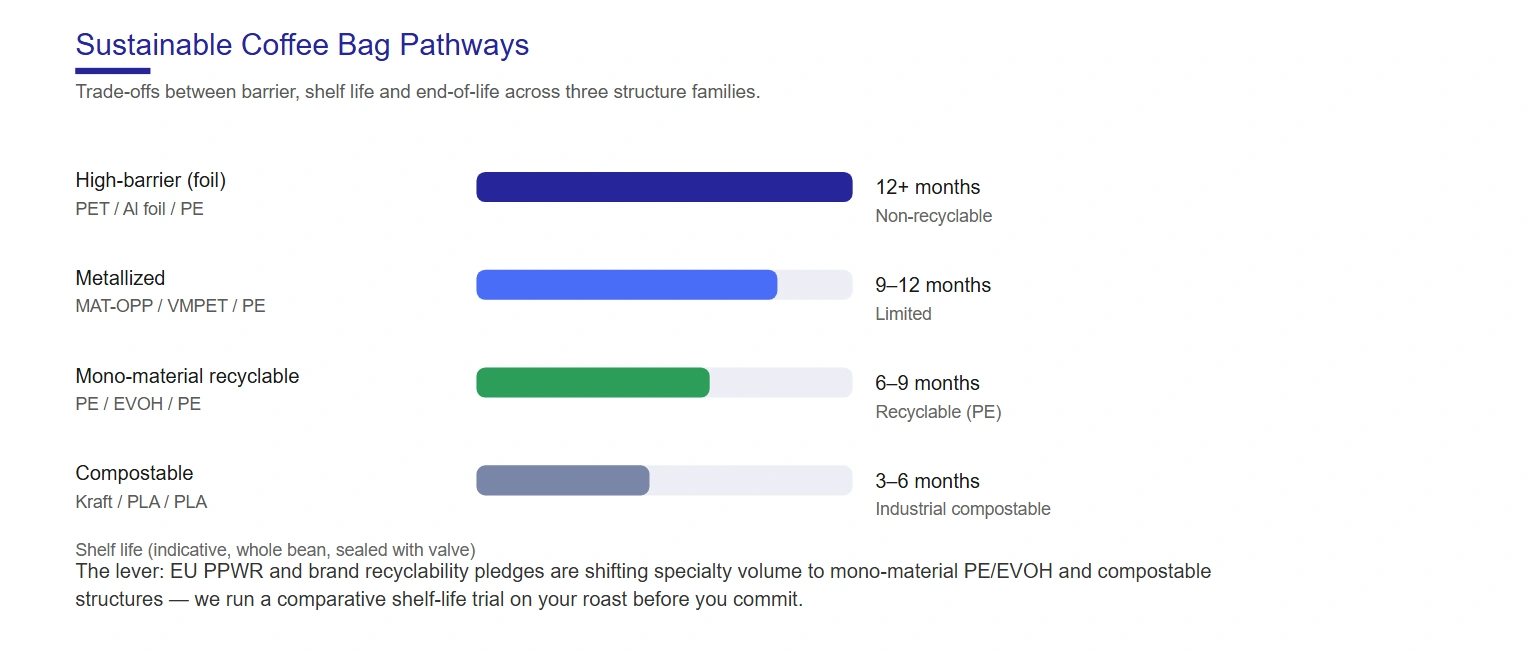
| Pathway | Structure | Shelf life | End-of-life | Trade-off |
|---|---|---|---|---|
| High-barrier (foil) | PET/Al/PE | 12+ months | Non-recyclable | Best protection, highest barrier |
| Metallized | MAT-OPP/VMPET/PE | 9–12 months | Limited (metallized film) | Balance of barrier & look |
| Mono-material recyclable | PE/EVOH/PE | 6–9 months | Recyclable (PE stream) | Slightly higher WVTR, premium cost |
| Compostable | Kraft/PLA or PLA/PLA | 3–6 months | Industrial compostable | Highest cost, shortest shelf life |
The fast-moving lever is the EU PPWR (EU 2025/40) and brand recyclability commitments: mono-material PE/EVOH coffee bags now achieve RecyClass approval while still carrying a one-way valve, and are the fastest-growing structure in the specialty segment. We can run a comparative shelf-life trial (foil vs. mono vs. compostable) on your exact roast before you commit.
Total Cost of Ownership vs. Rigid Coffee Packaging
| Cost driver | Flexible coffee bag | Rigid can / tin / jar |
|---|---|---|
| Unit packaging cost | Low — lightweight film | High — metal/glass + lid |
| Freight / warehousing | High cube efficiency, flat-fold pre-form | Heavy, low cube efficiency |
| Carbon footprint | Lower per unit | Higher per unit |
| Filling speed | High (VFFS / HFFS) | Slower (rigid handling) |
| Shelf life | 9–12+ months (with valve) | Long, but over-engineered for coffee |
| Branding surface | Full 360° print, no plate for digital | Limited to label |
The common mistake is comparing bag unit price alone. A 5% cheaper film that causes 1% line down-time or a burst bag in transit is a net loss — evaluate the bag as a system cost: barrier + valve + seal reliability + fill speed + freight, not film price per thousand.
Applications by Coffee Segment
- Specialty / third-wave roasters — flat-bottom & quad-seal, matte or soft-touch finish, pull-tab zipper, clear window, valve.
- Amazon & e-commerce sellers — hang hole, puncture-resistant structure for parcel shipping, nitrogen-flushed, sized to FBA dims.
- Subscription boxes — multi-SKU short runs, digital print with no plate fees, fast format changeovers.
- Private label & white label — low MOQ, quick artwork swap, consistent colour management across SKUs.
- Foodservice / wholesale — 2 lb & 5 lb side-gusset and quad-seal, tin-tie, high-volume pricing.
- Ground coffee & bricks — N2-flushed pillow/brick packs, stick packs and filter-pack tubing.
Customization Options
- Printing — rotogravure (high volume) or digital (low MOQ, no plate fees, full CMYK with gradients and photography).
- Finishes — matte, gloss, soft-touch, metallic, holographic, kraft/paper-touch, selective UV and spot varnish.
- Structure & barrier — foil, metallized, mono-material recyclable or compostable, sized to your shelf-life target.
- Features — valve (with/without filter), press-to-close or pull-tab zipper, tin-tie, tear notch, hang hole, clear window.
- Formats & sizes — any of the five formats, custom dimensions calculated from your fill weight and bean density.
Quality Control & Test Methodology
Every batch is tested against the standards below and we ship a certificate of analysis (CoA) on request. These are the tests a serious coffee bag supplier should be able to quote pass values for.
| Test | Standard | What it verifies | Typical pass spec |
|---|---|---|---|
| Oxygen transmission (OTR) | ASTM D3985 | Barrier to O2 (staleness) | Per structure (see barrier table) |
| Water vapour transmission (WVTR) | ASTM F1249 | Barrier to moisture | Per structure |
| Seal strength | ASTM F88 | Seal integrity | ≥ 20 N/15 mm (structure-dependent) |
| Hot tack | ASTM F1921 | Seal holds during fill | ≥ 3 N/15 mm |
| Coefficient of friction | ASTM D1894 | Machine runnability | 0.12–0.25 (film-to-metal) |
| Puncture resistance | ASTM F1306 / D5748 | Resistance to sharp bean edges | Per gauge spec |
| Valve leak / one-way function | Internal (pressure decay) | Valve vents CO2, no O2 ingress | Opens at crack pressure; zero backflow |
| Gauge / thickness | ASTM D6988 | Film thickness | ±3% of spec |
| Dyne / surface energy (print side) | ASTM D2578 | Ink adhesion | ≥ 38 dyn/cm |
| Burst test | Internal / ASTM F1140 | Bag integrity under pressure | Per format spec |
Failure Modes & Prevention
These are the failure modes we most often inherit from other suppliers’ bags. Ask a candidate supplier how they prevent each one — the answer separates a film converter from a coffee-packaging engineer.
| Failure mode | Root cause | Detection | Prevention |
|---|---|---|---|
| Bag ballooning / burst | Valve missing, wrong crack pressure, or sealing too soon after roast | Visual, burst test | Correct valve spec; seal within valve vent window |
| Premature staling | OTR too high for shelf-life target; flex-crack in metallized film | OTR test, taste panel | Upgrade barrier; add flex-crack allowance |
| Valve leak (O2 backflow) | Fouled/defective valve membrane or poor valve heat-seal | Pressure-decay / dye test | Filter valve for oily roasts; verify valve seal temp |
| Aroma / flavour loss | Weak seal, low barrier, or scented-film migration | Gas chromatography, sensory | Foil/heavy metallized; low-odour inks |
| Seal failure / leakers | Contamination in seal area (coffee dust, oil) | In-line vision, dye-penetrant | Seal-area cleanliness; wider seal; tuned dwell |
| Puncture in transit | Thin gauge + sharp bean edges + parcel handling | Drop test, puncture test | Thicker structure; add cushioning in mailers |
| Zipper failure | Wrong zipper type or misaligned notch | Cycle test | Pull-tab for flat-bottom; notch above zipper |
MOQ, Pricing Factors & Lead Time
| Factor | Impact |
|---|---|
| Order quantity | MOQ from 1,000 pieces (digital print); unit price falls steeply at 10k / 50k / 100k+ (rotogravure) |
| Print route | Digital = no plate fees, ideal for multi-SKU & <10k; rotogravure = lower unit cost at high volume |
| Structure | Compostable & mono-material cost more than metallized; foil mid; VMPET most economical |
| Features | Each add-on (valve, zipper, window, tin-tie) adds a fixed per-bag cost |
| Size / film weight | Larger bags & heavier gauges use more film |
| Finishes | Soft-touch, spot UV, holographic add cost vs. standard matte/gloss |
Lead time: free pre-production samples in 3–5 days; production 7–15 days after artwork approval (digital); rotogravure adds cylinder lead time. We hold standard valve and zipper inventory to avoid component delays.
Production Process
- Artwork & prepress — CMYK, PDF/vector, fonts outlined, 3 mm bleed; we check for registration and print feasibility.
- Plate / cylinder (rotogravure) or RIP (digital) — colour-managed to your brand standard.
- Printing & lamination — reverse-print on film, then solvent-free or solvent lamination of the barrier layers.
- Curing — laminate cure to full bond strength (≥ 2.5 N/15 mm T-peel) before slitting.
- Slitting & pouching — to width, then form (flat-bottom / quad-seal / side-gusset / stand-up / pillow).
- Valve, zipper & fitment application — in-line heat-seal of valves and zippers.
- QC & packing — in-line vision + batch testing (seal, OTR/WVTR, valve), then poly-packed and cartoned for export.
Coffee Bag Supplier Evaluation Checklist (15 Points)
- Do they state OTR/WVTR with test conditions, or just say “high barrier”?
- Can they specify valve crack pressure, filter type and body material?
- Do they offer recyclable mono-material and compostable structures, with certification?
- Do they provide a Declaration of Compliance and migration-test certificates per structure?
- Can they run a comparative shelf-life trial on your actual roast?
- What is their seal-strength and hot-tack test data?
- Do they have in-house pouching, or do they outsource (adds lead time & margin)?
- What is their flex-crack allowance for metallized film?
- Do they control COF for high-speed lines?
- What is their real MOQ and does digital print remove plate fees?
- Do they hold valve/zipper inventory to avoid component delays?
- What is their QC sampling plan (AQL) and can they ship a CoA?
- Do they understand MAP / nitrogen-flushing residual-oxygen targets?
- Can they match your existing bag exactly (reverse-engineer a sample)?
- Do they publish a failure-mode analysis and prevention plan?
Coffee Packaging Market Intelligence
The global coffee packaging market is a growing, consolidating segment. Independent market research pegs it at USD 910.9 million in 2025, reaching USD 1,388.1 million by 2034 at a 4.65% CAGR (IMARC Group), with a corroborating estimate of USD 919.85 million (2025) → USD 1,400.18 million (2034) at 4.78% CAGR (Fortune Business Insights). Within it, bags & pouches are the leading packaging segment by format. The narrower coffee-bags market is projected to grow from USD 0.7 billion (2026) to USD 1.2 billion (2036) at 5.0% CAGR (Future Market Insights).
- Specialty & third-wave growth — premiumization drives demand for flat-bottom, windowed, matte-finish bags with short runs.
- E-commerce & subscriptions — single-serve and multi-SKU programs shift volume toward digital-printed, quick-turn bags.
- Sustainability regulation — EU PPWR and brand recyclability pledges push mono-material and compostable structures.
- Single-serve & pods — stick packs and filter-pack tubing grow faster than bulk retail.
- Convenience reseal — zipper and pull-tab adoption rises as consumers re-open multiple times.
Frequently Asked Questions
Do freshly roasted coffee beans need a one-way degassing valve?
For whole-bean coffee sealed within 24–48 hours of roasting, yes — the CO2 the beans release will balloon or burst an unvented bag. A one-way valve vents that gas while blocking oxygen. For pre-ground, nitrogen-flushed brick packs sealed well after degassing, a valve is optional.
Which film structure best protects coffee aroma?
Foil (PET/Al/PE) gives the lowest OTR and WVTR and best aroma retention for 12+ month shelf life. Metallized MAT-OPP/VMPET/PE is the economical standard for 9–12 months. Recyclable mono-material PE/EVOH/PE suits 6–9 month programs with a sustainability mandate.
What is the minimum order quantity (MOQ)?
From 1,000 pieces on digital print (no plate fees). Unit cost drops sharply at 10k / 50k / 100k+ pieces where rotogravure becomes economical. Free pre-production samples ship in 3–5 days.
Can I get recyclable or compostable coffee bags?
Yes. Recyclable mono-material PE/EVOH/PE carries RecyClass approval, and Kraft/PLA structures are industrially compostable (EN 13432 / BPI / OK Compost). We run a comparative shelf-life trial on your roast before you commit.
What formats do you offer?
Flat-bottom (box), quad-seal, side-gusset, stand-up pouch and pillow/brick — plus roll-stock film and stick packs — sized from 100 g to 5 lb from your bean density.
Do you provide food-contact compliance documents?
Yes — a Declaration of Compliance and migration-test certificates for FDA 21 CFR 177.1520, EU 10/2011, GB 4806, REACH and Prop 65, per structure and batch.
How do you test quality?
Every batch is tested for OTR (ASTM D3985), WVTR (ASTM F1249), seal strength (F88), hot tack (F1921), COF (D1894), puncture (F1306) and valve one-way function, with a CoA on request.
Can you match a bag I already use?
Yes — send a sample and we reverse-engineer the structure, dimensions, barrier and valve, then quote a like-for-like or improved version.
Key Takeaways
- Specify barrier with numbers and conditions — OTR/WVTR without temperature/RH is not a spec.
- Treat the valve as a specified component — crack pressure, filter and seal-temperature window, not an afterthought.
- Match the bag to the fill line and the roast — structure, COF, hot-tack and valve all interact.
- Evaluate total cost of ownership — barrier + valve + seal reliability + fill speed + freight, not film price per thousand.
- Plan for sustainability now — PPWR and brand pledges are already moving volume to recyclable and compostable structures.
Get a Free Coffee Bag Sample & Quote
Tell us your format, fill weight, target shelf life, print route and sustainability goal — our engineers will return a structure recommendation with quantified barrier data and a quote within 24 hours. Free pre-production samples in 3–5 days.
You Also May Like
Ready to Improve Your Packaging Supply Chain?
Whether you are looking for a new packaging supplier, a backup manufacturer, or a trusted sourcing partner, We are ready to support your business.