Custom PVC Shrink Sleeves
— 360° Full-Body Shrink Labels for Bottles, Cans & Containers
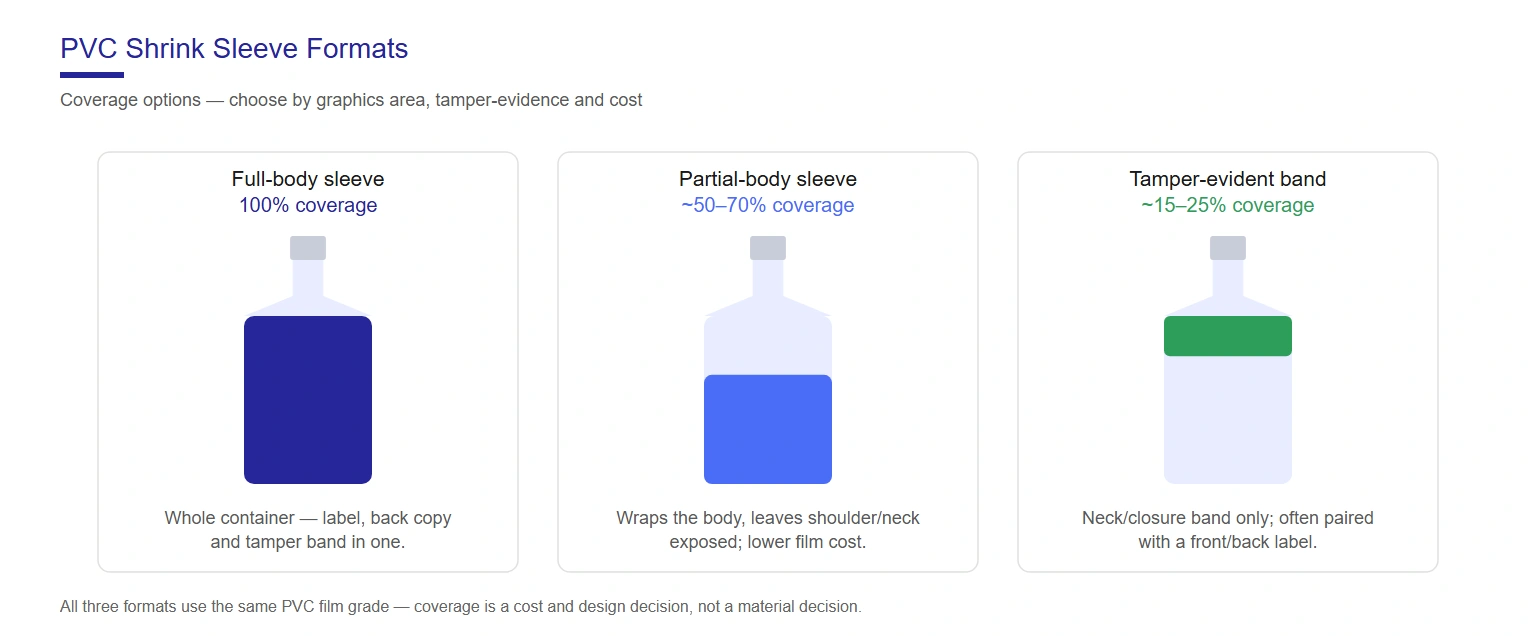
A PVC shrink sleeve is a heat-shrinkable, full-colour label film that is printed flat, solvent-seamed into a tube, dropped over a container and heat-shrunk to conform to any three-dimensional shape. It turns a plain bottle, jar, can or tube into a 360° branded billboard — with tamper evidence, product protection and maximum shelf impact — at the lowest film cost of any shrink-label material.
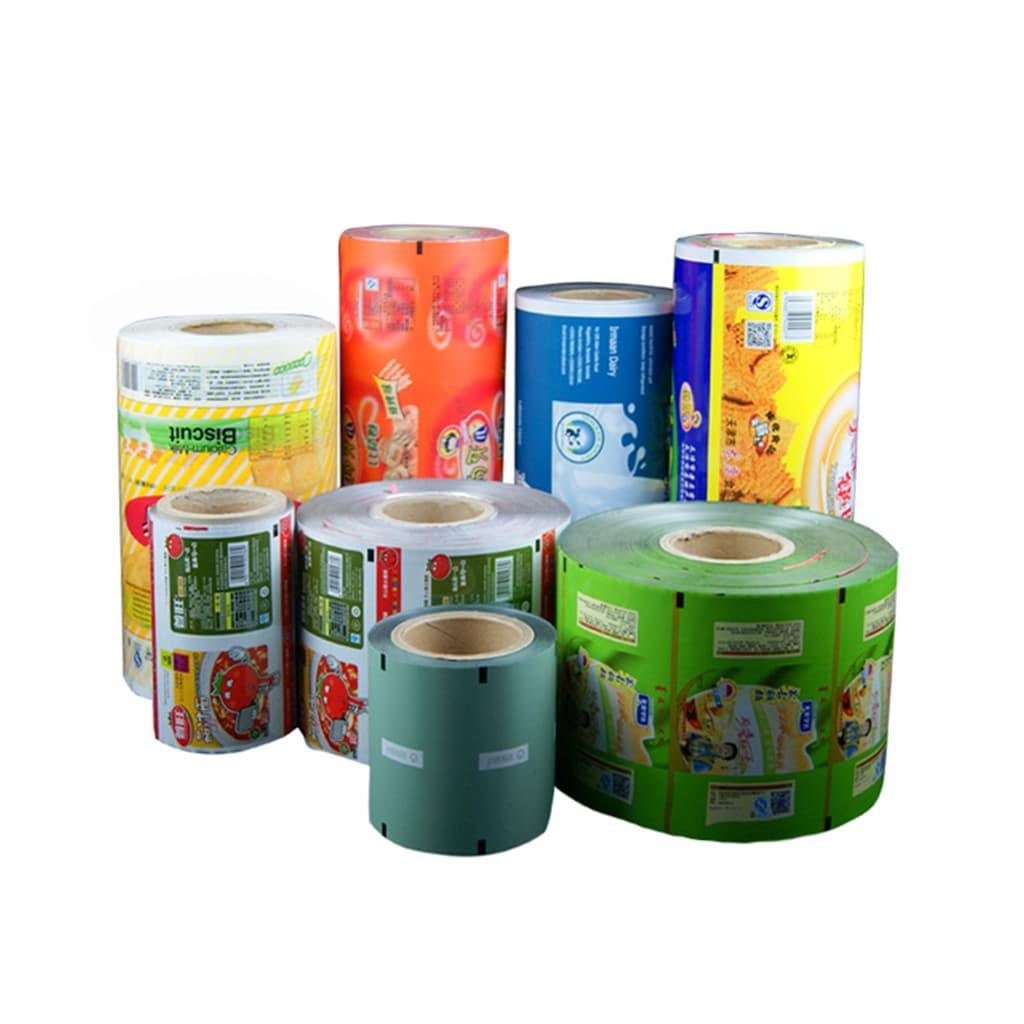
A PVC shrink sleeve (also called a shrink sleeve label or heat-shrink sleeve) is a tubular, uniaxially-oriented PVC film that is reverse-printed, seamed and heat-shrunk onto a container so it hugs every contour — including curved shoulders, waists, ribs and recessed panels that flat labels cannot cover. Because the sleeve wraps a full 360° and conforms in three dimensions, it replaces the label, the tamper-evident band and the back-panel copy in a single applied component. For packaging engineers it is the highest-graphics-yield-per-cost labelling method available today; for brand owners it is the fastest way to premiumise shelf presence; for procurement it is a lower-cost, single-SKU alternative to pressure-sensitive labels.
What you can expect from our factory
- ISO 9001:2015 quality-managed production with full batch and material traceability
- 10-colour rotogravure plus flexo and digital print — near-photographic 360° artwork
- 40–65% transverse shrink film, engineered for deep-draw and complex container profiles
- Compliance documentation on file: FDA 21 CFR, EU 10/2011, REACH, RoHS, California Prop 65, SGS
- Free pre-production sample in 5–7 days; MOQ from 10,000 sleeves per design
- 15–25 day lead time for repeat orders, with digital proofing before cylinder engraving
PVC Shrink Sleeve Anatomy: What Is Actually Inside the Film
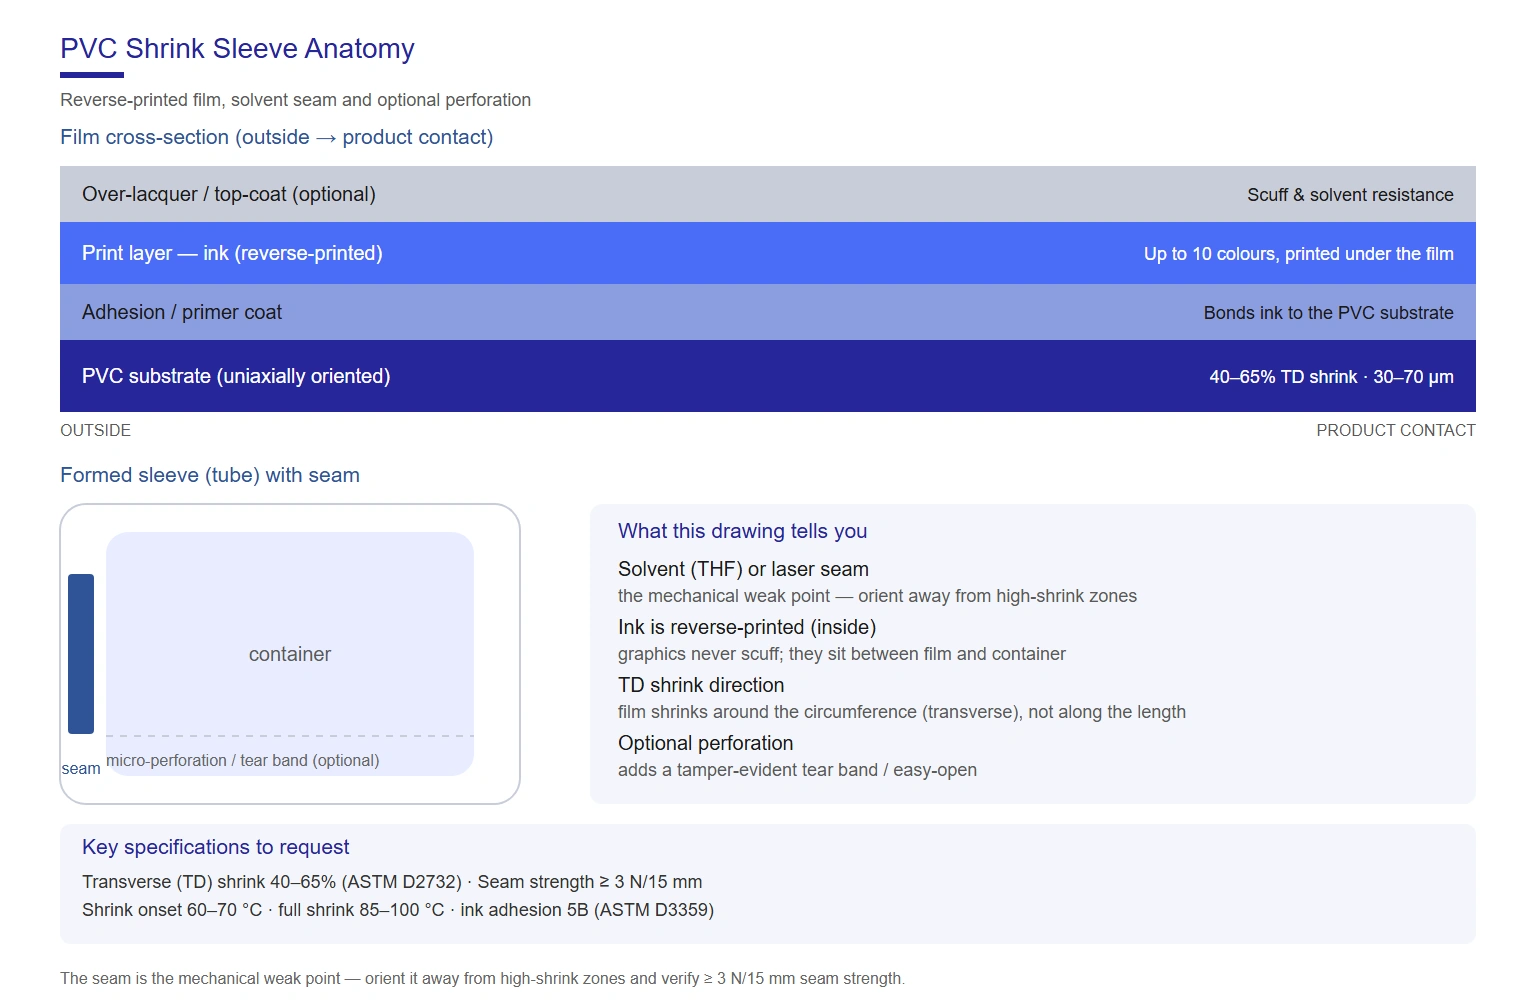
A shrink sleeve is not “ink on a plastic tube.” It is a deliberately engineered, layered assembly in which the artwork, the film’s orientation (shrink memory) and the seam must all be specified together — or the sleeve fails on the filler, not on the bench. The four functional layers, plus the seam and optional perforation, determine shrink %, print quality, seam strength and cost.
| Layer / Component | Function | What to specify |
|---|---|---|
| Print layer (ink) | Carries the 360° artwork; reverse-printed on the film’s inner surface so ink is protected under the film | Rotogravure / flexo / digital; ink system (solvent, UV or water-based); up to 10 colours; varnish or over-lacquer |
| Adhesion / primer coat | Bonds ink to the PVC substrate and prevents ink delamination during shrink | Primer type; ink-adhesion spec (pass 5B cross-cut, ASTM D3359) |
| PVC substrate film | Uniaxially-oriented (TD) PVC with built-in “shrink memory” released by heat | Thickness 30–70 µm; transverse shrink 40–65%; shrinkage force |
| Optional barrier / coating | Adds scuff resistance, solvent resistance or gloss | Top-coat / matte / soft-touch; coefficient of friction (COF) |
| Seam | Welds the flat film into a tube; the mechanical weak point of every sleeve | Solvent (THF) seam or laser seam; seam width; seam strength ≥3 N/15 mm |
| Optional perforation | Micro-perforation or tear tape enables easy opening / tamper evidence | Perforation pattern, tear strength, tamper-evident neck band design |
The single most important specification is the transverse (TD) shrink ratio: it must match the maximum circumference reduction of your container. A sleeve specified at 40% shrink cannot reliably conform a bottle whose shoulder is 55% narrower than its body — the film will bridge, wrinkle or split. Select the shrink % from the container’s worst-case draw-down, not its average.
Material Selection: PVC vs PETG vs OPS vs PLA Shrink Films
PVC is the volume workhorse of shrink labels, but it is one of four mainstream shrink-film materials and the wrong choice in the wrong application. The table below is the engineering decision matrix our team uses with every new project. Read it against your two hard constraints — maximum required shrink % and recycling/recyclability policy — not against unit price alone.
| Property | PVC | PETG | OPS | PLA |
|---|---|---|---|---|
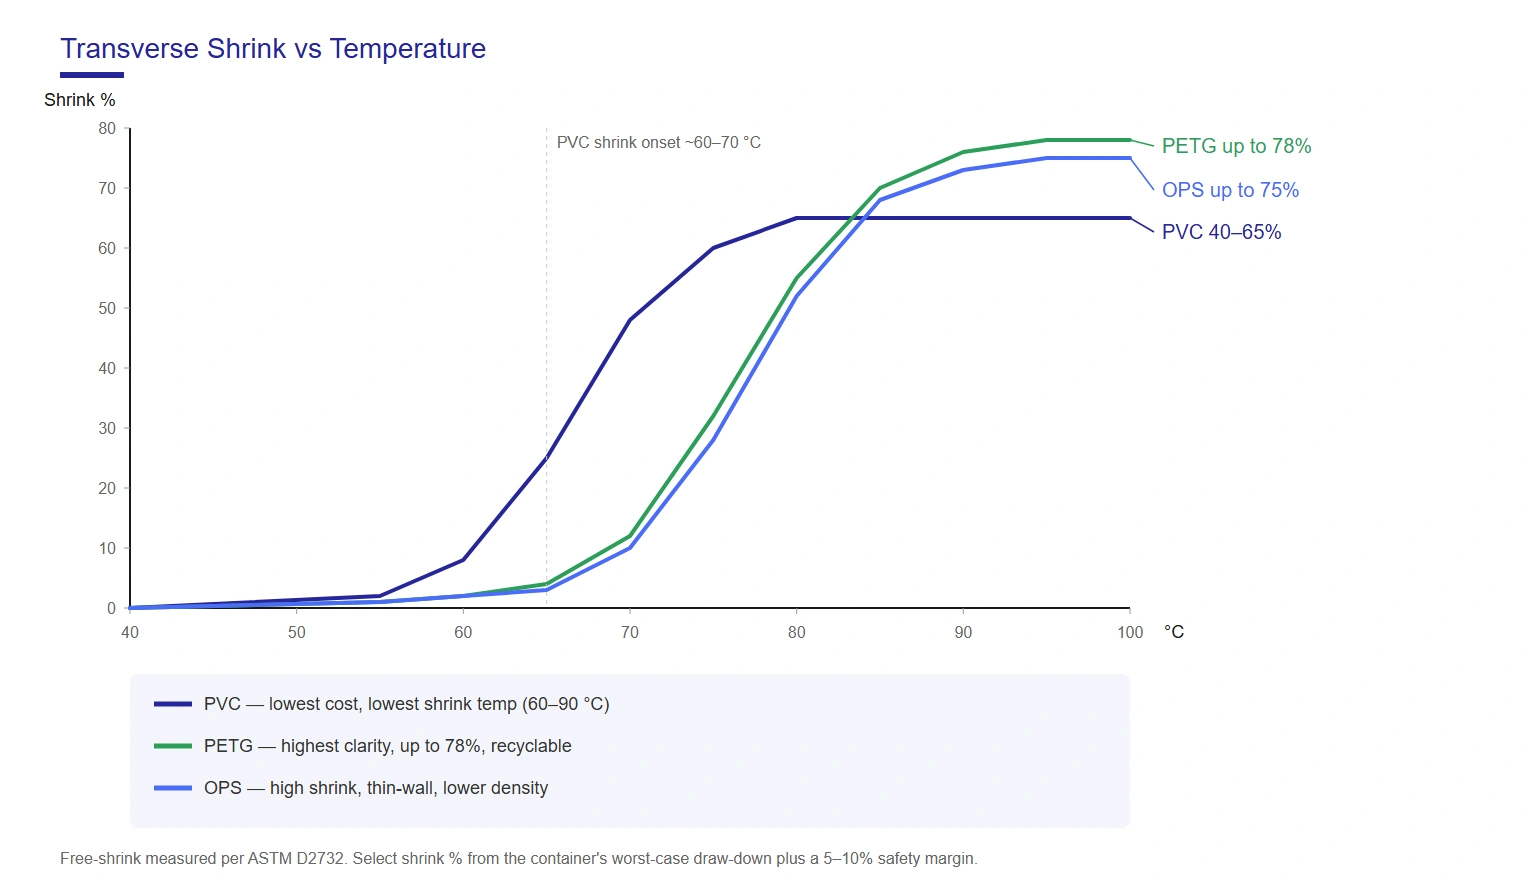
| Max transverse shrink | 40–65% | up to 78% | up to 75% | 50–75% |
| Shrink temperature | 60–90°C (lowest) | 70–100°C | 70–95°C | 60–95°C |
| Clarity / gloss | Good (slight haze) | Excellent (glass-like) | Good | Good |
| Relative film cost | Lowest | Mid–high | Low–mid | Highest |
| Density | 1.35–1.40 g/cm³ | 1.27 g/cm³ | 1.05 g/cm³ | 1.24 g/cm³ |
| Recyclability | Poor — chlorine contaminates PET stream | Good — crystallisable PETG is APR-approved | Limited | Compostable (industrial); not drop-in recyclable |
| Best use | Cost-sensitive FMCG, deep-draw shapes | Premium beverages, recyclable packaging | High-shrink thin-wall shapes | Eco-positioned brands |
Why brands still choose PVC: the lowest film cost, the lowest shrink-onset temperature (faster, lower-energy tunnels) and excellent print receptivity on gravure. Why some brands are moving off PVC: its chlorine content makes it a “detrimental contaminant” in the PET recycling stream, and a number of global brands have published PVC-elimination roadmaps. See the sustainability section below for the full picture — and note that a crystallisable PETG sleeve is often a drop-in alternative when a recycling mandate applies.
PVC Shrink Film Technical Specifications
These are the numbers a packaging engineer needs to qualify a PVC shrink sleeve. All values are for our standard 40–65% TD-shrink PVC shrink film; other grades are available on request. Test conditions follow the ASTM/ISO methods in the QC section below.
| Parameter | Typical value | Unit / method |
|---|---|---|
| Film thickness | 30 – 70 (standard 40–50) | µm (ASTM D6988) |
| Transverse (TD) shrink | 40 – 65 | % free shrink (ASTM D2732) |
| Machine (MD) shrink | 0 – 8 | % (ASTM D2732) |
| Shrink onset temperature | 60 – 70 | °C |
| Full-shrink temperature (film) | 85 – 100 | °C (tunnel air 130–160°C) |
| Tensile strength (MD) | 40 – 60 | MPa (ASTM D882) |
| Elongation at break | 200 – 400 | % (ASTM D882) |
| Haze | ≤ 5 | % (ASTM D1003) |
| Gloss (60°) | ≥ 85 | GU (ASTM D2457) |
| Coefficient of friction | 0.2 – 0.4 | kinetic (ASTM D1894) |
| Density | 1.35 – 1.40 | g/cm³ |
| Seam strength | ≥ 3 | N / 15 mm (seam peel) |
| Ink adhesion | 5B (no removal) | ASTM D3359 cross-cut tape test |
| Surface energy (print side) | ≥ 38 | dyn/cm (ASTM D2578) |
How a PVC Shrink Sleeve Is Applied: The Heat-Shrink Process
On the filling line the pre-formed sleeve is opened, placed over the container, and passed through a hot-air or steam shrink tunnel. The oriented film relaxes back toward its pre-orientation dimensions, tightening around the container. Three variables control the result — tunnel temperature, residence time and air/steam distribution — and they must be tuned to the film’s shrink curve, not guessed.
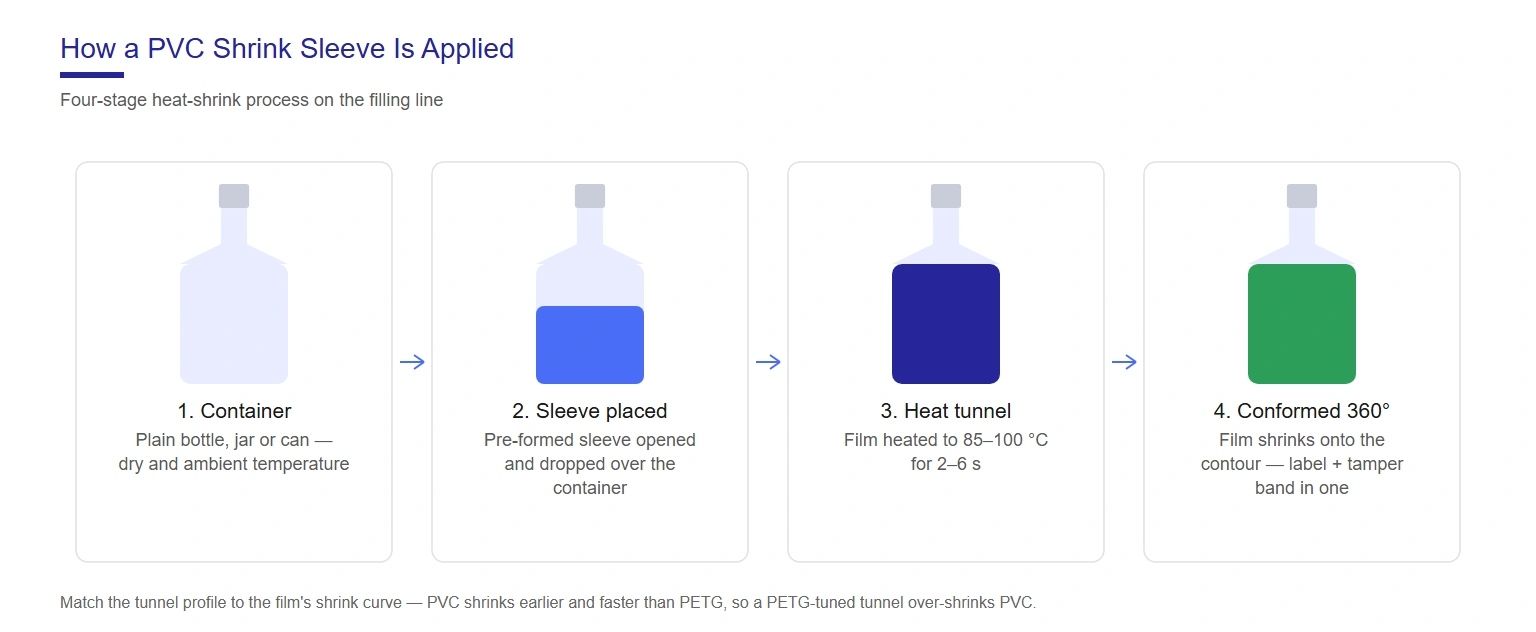
- Container preparation — the container must be dry and at ambient temperature; condensation causes uneven shrink and “ghosting”.
- Sleeve opening & placement — a mandrel opens the sleeve; it is positioned so the perforation/tear band sits at the correct height.
- Heat exposure — hot-air or steam tunnel heats the film to 85–100°C (film temp); residence time 2–6 s depending on tunnel length.
- Conformity & set — the film shrinks onto the contour and cools, locking graphics in place; residual shrink <5% must remain for on-shelf stability.
- Inspection — vision systems check seam position, distortion, bridging and label height before palletising.
A common failure is running a PVC sleeve through a PETG-tuned tunnel: PVC shrinks earlier and faster, so a tunnel set for PETG will over-shrink, wrinkle or split PVC. Always match the tunnel profile to the film’s shrink curve.
Print Technology: Rotogravure, Flexo and Digital
Shrink sleeves are printed flat, reverse-printed (artwork on the inside), and then seamed — so the ink is sandwiched between film and container and never scuffs. Print method is a cost-versus-run-length decision:
| Print method | Run length | Colour depth | Cost structure | Notes |
|---|---|---|---|---|
| Rotogravure | 50,000+ sleeves (long runs) | Up to 10–12 colours, photorealistic | High cylinder engraving cost, lowest per-unit ink cost | Standard for beverages & FMCG; near-photographic gradients |
| Flexographic | 10,000–100,000 (mid runs) | Up to 10 colours, solid & spot | Lower plate cost, faster changeover | Good for spot-colour brand work and shorter seasonal runs |
| Digital (HP Indigo etc.) | 1–10,000 (short runs / variable data) | Full process colour, variable data | No plates, highest per-unit cost | Ideal for SKU proliferation, test markets, sequential numbering |
Ink system matters as much as print method. Solvent-based inks (standard) deliver the widest shrink performance and adhesion; UV inks cure instantly but can crack on deep-draw areas if not formulated for high elongation; water-based inks are the low-VOC option for sustainability programmes. We specify the ink to the film’s shrink % — an ink that passes at 40% shrink may crack at 65%.
Applications by Industry
PVC shrink sleeves are the default labelling technology wherever 360° graphics, contour conformity, tamper evidence and low unit cost must coexist:
- Beverages — bottled water, juices, RTD tea/coffee, energy drinks, dairy, craft beer cans and spirit bottles
- Food & condiments — sauces, dressings, honey, edible oil, snack multi-packs
- Personal & home care — shampoo, body wash, detergent, cleaning and automotive care bottles
- Cosmetics & beauty — lotions, serums, hair care and fragrance packaging
- Nutraceuticals, pharma & CBD — supplement bottles, tinctures, tamper-evident and compliance copy
- Multi-packs & promotional — 2-for-1 bottle bundling, gift sets, limited-edition wraps
Regulatory & Compliance Matrix
PVC food-contact compliance centres on monomer/plasticiser migration limits and on the phthalate restrictions that apply to flexible PVC. Confirm the matrix below against your target market before releasing a design:
| Regulation | Scope | Relevance to PVC shrink sleeves |
|---|---|---|
| FDA 21 CFR 177.1210 / 175.300 | USA — food-contact polymers & coatings | Sets extractables limits for PVC and its plasticisers in food-contact closures/labels |
| EU 10/2011 (EC 1935/2004) | EU — plastics food contact | Overall migration limit 10 mg/dm²; specific migration limits (SML) for PVC additives |
| REACH Annex XVII (EC 1907/2006) | EU — restricted substances | Restricts phthalates DEHP/DBP/BBP/DIBP (≤0.1%) in articles |
| California Proposition 65 | USA (CA) — exposure warnings | Phthalates and lead listed; requires label if exposure limits exceeded |
| RoHS Directive (2011/65/EU) | EU — electronics | Restricts lead/cadmium/phthalates; relevant for electronics-promo sleeves |
| BRCGS Packaging (Issue 6) / ISO 22000 | Global — food-safety management | Certified hygiene and contamination control in sleeve manufacture |
We supply full migration-test and phthalate-declaration documentation (SGS-tested) with every food-contact order, and can formulate phthalate-free plasticiser systems on request for brands with a “PVC-free or phthalate-free” policy.
Sustainability & the PVC-to-PETG Migration
This is the section your competitors skip — and the one that decides whether your shrink-label programme survives a recycling audit. PVC sleeves are functionally excellent but environmentally constrained: their chlorine content classifies them as a “detrimental contaminant” in the PET bottle recycling stream, where even a small PVC fraction degrades recycled-PET clarity and triggers hazardous by-products during re-melt. As a result, the APR (Association of Plastic Recyclers) design guidance and RecyClass have driven a broad industry shift toward recyclable-friendly shrink films.
- Recycling contamination — PVC sinks in the PET float-sink separation, but residual PVC raises chlorine in RPET; brands increasingly exclude PVC sleeves from PET packaging.
- APR / RecyClass guidance — crystallisable PETG and some OPS/PE structures are approved as “recycle-ready” for PET bottles; PVC is not.
- Brand roadmaps — multiple global beverage and home-care brands have published PVC-elimination targets, pulling volume toward PETG, OPS and PLA.
- The pragmatic position — for non-PET containers (glass, HDPE, metal), PVC remains an excellent, compliant, low-cost choice; for PET bottles destined for closed-loop recycling, specify crystallisable PETG.
We advise on both paths: PVC where cost and deep-draw performance win, and crystallisable PETG/OPS/PLA where a recycling or brand mandate applies. Ask us for a material-sustainability comparison mapped to your specific container and market.
Total Cost of Ownership: PVC vs PETG vs Self-Adhesive Labels
Unit film price is the wrong number to optimise. A 5% cheaper film that halves line speed or adds a label-inspection step costs far more than it saves. Compare on total applied cost:
| Cost driver | PVC sleeve | PETG sleeve | Self-adhesive label |
|---|---|---|---|
| Film / labelstock cost | Lowest | Mid–high | Highest (liner + adhesive) |
| Print & plate cost | Gravure cylinders (amortised over long runs) | Same as PVC | Low (digital/flexo, no cylinders) |
| Application line speed | High (600–1000 bpm achievable) | High (slightly slower tunnel) | High but liner-waste handling |
| 360° coverage (no second label) | Yes — one component | Yes — one component | No — front/back = two labels |
| Tamper evidence | Built-in (neck band) | Built-in | Separate component required |
| Best-fit run length | ≥50,000 (cylinder amortisation) | ≥50,000 | Any (incl. very short runs) |
Rule of thumb: below roughly 10,000–20,000 sleeves per SKU the gravure cylinder cost dominates and digital or self-adhesive wins; above it, PVC sleeves deliver the lowest cost per labelled unit of any 360° method.
Failure Modes & Prevention (No Competitor Publishes This)
These are the seven ways a PVC shrink sleeve fails in the field, what causes each, how we detect it in QC, and how we prevent it. Use it as your incoming-inspection checklist.
| Failure mode | Root cause | Detection | Prevention |
|---|---|---|---|
| Ink cracking / crazing | Ink film too thick or low-elongation ink on high-shrink (65%) areas | Visual + stretch test after shrink | High-elongation ink system; ink-formulation matched to shrink % |
| Seam splitting | Insufficient solvent dwell, seam contamination, over-shrink | Seam peel test (≥3 N/15 mm) | Controlled seam width & solvent; seam orientation away from draw-down |
| Graphics distortion | Artwork not compensated for TD shrink; wrong orientation | Distortion grid / proof shrink | Pre-distortion artwork from a printed shrink trial |
| Bridging / tunneling | Shrink % below container draw-down; low shrink force | Worst-case profile trial | Specify shrink % from max draw-down, not average |
| Wrinkles / uneven shrink | Tunnel temp or airflow too high/uneven | Tunnel profile audit | Match tunnel to film shrink curve; even air/steam distribution |
| Blocking (sleeves sticking) | COF too low + static in storage | COF (ASTM D1894) + static check | Anti-block additive / static control; correct winding tension |
| Plasticiser migration | PVC additive migrating to surface/product | Migration test (SGS) | Food-grade / phthalate-free plasticiser formulation |
QC & Test Methodology
Every batch is tested to the methods below before release. We share certificates of analysis on request — and we encourage buyers to run the same tests on incoming stock.
| Test | Standard | What it verifies | Pass spec |
|---|---|---|---|
| Free shrink | ASTM D2732 | TD / MD shrinkage at temperature | 40–65% TD (as specified) |
| Shrink force / shrink tension | Internal (oil-bath) | Conformity force on the container | As per profile |
| Coefficient of friction | ASTM D1894 / ISO 8295 | Sleeve feed & application slip | Kinetic 0.2–0.4 |
| Tensile & elongation | ASTM D882 | Film strength and stretch | MD 40–60 MPa; 200–400% |
| Haze / transparency | ASTM D1003 | Optical clarity | ≤5% |
| Gloss (60°) | ASTM D2457 | Surface gloss | ≥85 GU |
| Thickness | ASTM D6988 / ISO 4593 | Gauge consistency | ±3% |
| Ink adhesion | ASTM D3359 (cross-cut) | Ink-to-film bond | 5B — no removal |
| Seam strength | Seam peel (internal) | Seam weld integrity | ≥3 N / 15 mm |
| Surface energy | ASTM D2578 | Print-side wetting | ≥38 dyn/cm |
MOQ, Pricing Factors & Lead Time
PVC shrink sleeves carry a gravure cylinder cost per design (one cylinder per colour), which is why MOQ is higher than a simple pouch. Digital printing removes the cylinder cost and lowers MOQ for short runs and test markets.
| Item | Rotogravure (standard) | Digital (short run) |
|---|---|---|
| MOQ | 10,000 sleeves / design | 1,000 sleeves / design |
| Cylinder / plate cost | Per colour (one-time) | None |
| Sampling | 5–7 days (digital proof) | 3–5 days |
| Production lead time | 15–25 days | 7–12 days |
| Per-unit cost at scale | Lowest | Higher |
- Primary cost drivers: film gauge (thickness), number of print colours, shrink % grade, sleeve dimensions, and run quantity.
- Volume pricing: unit cost falls sharply at 100,000+ sleeves per SKU as cylinder and setup costs amortise.
- Repeat orders: cylinders are stored on file, so re-orders skip engraving and shorten lead time to 10–15 days.
Production Process
- Artwork pre-press & distortion — artwork is digitally pre-distorted to compensate for TD shrink so the printed graphic appears undistorted after shrinking.
- Cylinder engraving (gravure) — each colour is laser-engraved onto a gravure cylinder; digital files skip this step.
- Printing — the PVC film is reverse-printed on a rotogravure or flexo press with in-line varnish and solvent recovery.
- Slitting — the printed master roll is slit to the sleeve’s lay-flat width.
- Seaming — the flat film is formed into a tube and the overlap is solvent- or laser-seamed; perforation / tear tape is added if specified.
- Inspection & rewinding — vision inspection for print defects, seam position and splices; rewind to the specified roll length and core.
- Packing & shipping — rolls are PE-wrapped, boxed and labelled with batch traceability before export.
Supplier Evaluation Checklist (18 Points)
Score any shrink-sleeve supplier against these 18 points before committing volume. Most B2B competitors will not volunteer answers to more than half of them.
- Is the factory ISO 9001 (and BRCGS Packaging if food-contact) certified?
- Can they print 10+ colours rotogravure, or only flexo/digital?
- Do they reverse-print (ink under film) to prevent scuffing?
- Can they supply 40–65% TD shrink film with a documented shrink curve?
- Do they run a physical shrink trial on your actual container, not a generic sample?
- Is artwork digitally pre-distorted for shrink, with a proof you approve before cylinders?
- Do they document ink-adhesion (D3359) and seam-strength test results?
- Can they provide SGS phthalate / migration test reports for food contact?
- Do they offer phthalate-free and low-VOC (water-based) ink formulations?
- Can they advise on PVC vs crystallisable PETG/OPS/PLA for your recycling mandate?
- What is the MOQ and is there a digital short-run path for test markets?
- Are gravure cylinders stored for repeat orders, and at what re-order lead time?
- Do they offer tamper-evident perforation and tear-tape options?
- What is their QC sampling plan (AQL) and do they ship a certificate of analysis?
- Can they match a Pantone spot colour and hold it across batches?
- Do they provide roll-length, core and winding specs that match your applicator?
- What are their payment terms, and is there export/incoterm experience to your region?
- Can they provide 2–3 reference customers in your category?
Market Intelligence
The global shrink sleeve labels market was valued at USD 15.20 billion in 2025 and is projected to reach USD 22.43 billion by 2036, expanding at a 3.6% CAGR (2026–2036), according to Future Market Insights — an incremental opportunity of roughly USD 6.68 billion. Growth is being pulled by premiumisation in beverages, single-serve and on-the-go formats, and the transition from rigid secondary packaging to lightweight sleeves. See also Grand View Research and Mordor Intelligence for corroborating market sizing.
- Premiumisation — craft beer, RTD spirits and premium water brands use full-body sleeves as a low-cost route to shelf differentiation.
- Tamper-evidence & safety — regulatory pressure for tamper-evident and anti-counterfeit packaging favours full-body + neck-band sleeves.
- Sustainability migration — PVC-to-PETG/OPS/PLA substitution is the defining structural shift, driving product-mix change rather than volume decline.
- E-commerce & private label — Amazon sellers and private-label brands use short-run digital sleeves for SKU proliferation and test markets.
- Regional growth — Asia-Pacific leads volume; mature markets shift toward recyclable materials and automation.
Frequently Asked Questions
What is the minimum order quantity for custom PVC shrink sleeves?
MOQ is 10,000 sleeves per design for rotogravure printing (driven by the per-colour cylinder cost), and 1,000 sleeves for digital printing where we skip the cylinders entirely. For a first order we recommend a digital proof and a physical shrink trial on your container before committing to cylinders.
What shrink ratio do I need for my container?
Measure the largest circumference and the narrowest circumference your sleeve must cover; the required transverse shrink is that reduction expressed as a percentage, plus a 5–10% safety margin. Our standard PVC film covers 40–65% TD shrink, which handles most bottle shoulders and waists; we specify the exact grade from a trial on your container.
Is PVC shrink film food-contact safe?
Yes — when manufactured with food-grade PVC and compliant plasticisers. We supply FDA 21 CFR, EU 10/2011 and SGS migration documentation, and can formulate phthalate-free systems on request. Confirm your target market’s specific migration and phthalate limits with us before releasing a design.
Can I print photographic images and gradients on a shrink sleeve?
Yes. Rotogravure reproduces near-photographic images and smooth gradients across up to 10–12 colours. Because artwork is reverse-printed and pre-distorted for shrink, the finished graphic appears undistorted on the container — we run a printed shrink trial so you can approve the result before production.
How do you prevent the label from wrinkling or splitting on the line?
We match the film’s shrink curve to your tunnel profile, specify shrink % from the container’s worst-case draw-down (not the average), orient the seam away from high-shrink zones, and use high-elongation inks on deep-draw areas. We also share the tunnel temperature/residence-time recipe your line should run.
What is the difference between PVC and PETG shrink sleeves?
PVC offers the lowest film cost and lowest shrink temperature (60–90°C) but contains chlorine and is a “detrimental” contaminant in PET recycling. PETG offers higher clarity, up to 78% shrink, and recyclability (crystallisable grades are APR-approved) at a higher cost. If your container is PET and destined for closed-loop recycling, we recommend crystallisable PETG; for glass, HDPE or metal containers, PVC remains an excellent low-cost choice.
Can you add tamper-evident perforation or a tear band?
Yes. We add micro-perforation, a horizontal tear-tape, or a full tamper-evident neck band so the consumer can see and remove the seal cleanly. Specify the tear-strength and perforation pattern you want and we will engineer it to open consistently without weakening the sleeve during shrink.
What is the production and delivery lead time?
Digital proofs ship in 5–7 days and short-run digital production in 7–12 days. Rotogravure production takes 15–25 days from artwork approval (cylinder engraving included); repeat orders skip engraving and run 10–15 days. We confirm a delivery date before you commit and provide export/incoterm documentation.
Do you ship internationally and what are the logistics?
Yes — we export to 30+ countries by sea and air, with full incoterm and customs documentation. Sleeves ship as rewound rolls on cores matched to your applicator; we pack to protect against transit compression and static. Tell us your destination port and we will quote freight alongside the unit price.
Key Takeaways
- A PVC shrink sleeve is the lowest-cost 360° labelling method — one component replaces label + tamper band + back-panel copy.
- The critical specification is transverse shrink % (40–65%), chosen from the container’s worst-case draw-down, not its average.
- Match the tunnel profile to the film’s shrink curve; PVC shrinks earlier and faster than PETG — a mismatch wrinkles or splits the sleeve.
- Reverse-printing puts the ink under the film so graphics never scuff; rotogravure gives near-photographic 10-colour output.
- Watch the seam — it is the mechanical weak point; demand ≥3 N/15 mm seam strength and a documented test.
- For PET containers in closed-loop recycling, specify crystallisable PETG; for glass/HDPE/metal, PVC remains the low-cost workhorse.
- Demand compliance documentation (FDA, EU 10/2011, SGS phthalate/migration) and a physical shrink trial on your container before volume.
Specify Your PVC Shrink Sleeves
Send us your container drawing (or a sample), the artwork file, and your target market — our engineers will return a film, shrink %, print and seam recommendation with a digital proof and quotation within one business day. We ship a free pre-production sample in 5–7 days so you can validate shrink, graphics and line speed on your own filler before you commit to cylinders.
You Also May Like
Ready to Improve Your Packaging Supply Chain?
Whether you are looking for a new packaging supplier, a backup manufacturer, or a trusted sourcing partner, We are ready to support your business.